Precision Screen Printed & Knitted Apparel Range
Explore our premium core inventory engineered for private label branding, promotional merch, and luxury streetwear fashion lines. Click below for factory-direct wholesale pricing.
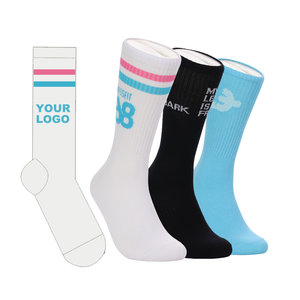
Custom Socks Factory Custom No Minimum Order High Quality Cotton White Socks Custom Socks With logo
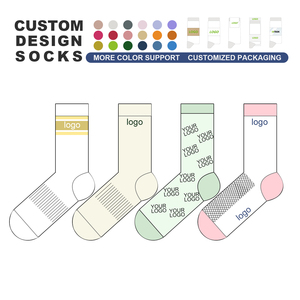
Custom Design Cotton Socken Personalized Logo Embroidered Men Tube Fashion Socks Sox Crew Dress Socks Stock Lot
Unisex Crew Personalized Design Your Own Logo Sock Customized Socks Jacquard Custom Logo Socks Low MOQ
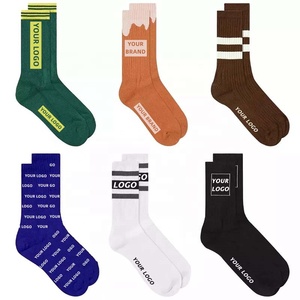
Designer Jacquard Knitted Crew 100% Cotton Thick Anti-Bacterial Brands Socks Casual Letter Bottom Logo Funny Sports Custom
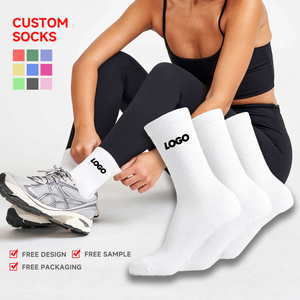
Personalized White Letter Socks Custom Logo Gym Crew Socks for Women Embroidery Sport Athletic Cotton Socks
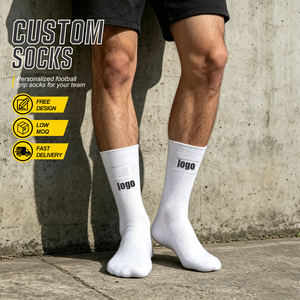
Breathable Sports Basketball Crew Men Socks Custom Socks Logo Sport Socks Running
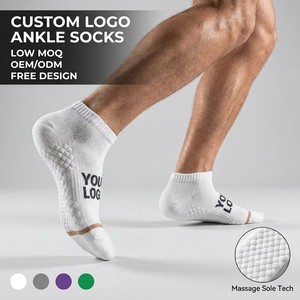
Custom Logo Massage Ankle Socks Anti-Blister Cotton Breathable Low-Cut Luxury Gift Hotel Amenity
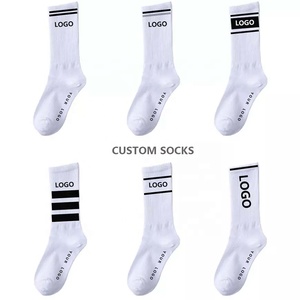
OEM Moq Fast Sample Oem Custom Logo Crew Socks Men Running Sport Socks, Cycle Athletic Custom Logo Basketball Socks
UK Screen Printing Manufacturing Landscape: Industry Strategic Analysis
The apparel manufacturing landscape in the United Kingdom has undergone a fundamental paradigm shift. As modern e-commerce apparel brands, UK-based fashion houses, and corporate enterprise buyers seek faster speed-to-market and nearshore resilience, selecting an authoritative, high-precision Screen Printing Manufacturer & Factory in the United Kingdom has become a mission-critical business decision. Traditional overseas supply chains frequently present UK business owners with catastrophic lead-time vulnerabilities, hidden tariff surcharges, unstable wash-fastness durability, and inflexible minimum order quantities (MOQs).
Modern textile screen printing is no longer a simple application of ink onto fabric; it is an exact chemical, mechanical, and artistic engineering discipline. From high-density plastisol prints for streetwear fashion in Soho and Shoreditch to zero-feel water-based discharge printing for eco-conscious UK corporate merchandise, selecting a production partner requires deep technical evaluation. Our operations bridge high-capacity manufacturing hubs with localized UK client management, offering custom cut-and-sew garment construction, bespoke private labeling, Pantone-matched screen printing, and specialized embroidery services optimized for British apparel sellers.
Advanced Ink Chemistry
Mastery of GOTS-certified water-based inks, high-density 3D puff additives, reflective metallic foils, and discharge chemistry ensuring soft-hand feel and superior wash resilience past 50+ industrial cycles.
Full-Package Cut & Sew
Going beyond blank garment printing. We build apparel from raw knitted rolls, including custom pattern grading, fabric weight matching (180 GSM to 500 GSM heavy fleece), custom neck tags, and branded poly bags.
Strict AQL 2.5 Quality Inspection
Every single print run undergoes rigorous tensile strength testing, seam pull verification, wash-shrinkage checking, and precise colorimeter Pantone verification prior to final packing.
Technical Screen Printing Methods: Technical Gain & Ink Engineering
Achieving commercial success in the UK apparel sector demands a nuanced understanding of textile decoration substrates and chemical ink formulations. Standard commercial screen printing utilizes fine mesh screens stretched over precision aluminum frames to force ink deposits onto garment panels. However, the physical interaction between cotton fibers, synthetic polyester blends, and ink vehicle systems dictates the visual finish, tactile hand-feel, and longevity of the garment.
1. Water-Based & Eco-Discharge Printing
Water-based inks utilize water as the primary solvent carrier for pigment particles. Unlike traditional heavy plastisol, water-based printing penetrates deep into the textile fibers rather than creating a rubbery coating on top of the fabric. For dark 100% cotton garments, our factories utilize Discharge Screen Printing. This technique uses an activating agent that removes the natural reactive dye from the raw cotton fiber and replaces it with custom Pantone pigments. The result is an ultra-soft, zero-feel print that breathes naturally—a mandatory requirement for luxury streetwear, high-end loungewear, and premium corporate merchandise across the UK and European Union markets.
2. High-Density Plastisol & Specialty 3D Puff Printing
For vibrant graphics requiring absolute opacity on dark synthetic blends, heavy cotton t-shirts, and 450 GSM heavyweight fleece hoodies, Plastisol remains the global industry standard. Formulated without phthalates or harmful chemicals, our modern plastisol inks provide extreme color fidelity across high-contrast artwork. To create tangible visual depth, we incorporate specialized 3D Puff additives and high-density screens. When cured through our industrial gas infrared tunnels at exact temperatures (320°F / 160°C), the ink expands vertically, creating crisp, tactile raised lettering and structural branding elements that instantly elevate garment retail values.
3. Metallic Foils, Silicone, & Reflective Inks
Modern athletic wear and high-fashion brands in London, Manchester, and Birmingham frequently request specialized performance finishes. We engineer custom silicone screen printing for elastane-heavy activewear and leggings, delivering high-stretch recovery without cracking or peeling. Additionally, glass-bead reflective inks (EN ISO 20471 compliant) provide ambient light reflection for urban night-running gear and tactical apparel, while heat-transferred metallic foil layers offer metallic luster for luxury accents.
Screen Printing Ink Selection & Substrate Compatibility
Compare screen printing methodologies to match your specific garment GSM, fabric composition, and target price point.
| Printing Technique | Optimal Fabric Substrate | Tactile Hand-Feel | Pantone Match Accuracy | Wash Durability (Cycles) | Recommended UK Application |
|---|---|---|---|---|---|
| Water-Based Ink | 100% Combed Organic Cotton | Ultra-Soft / Breathable | 98% Match Ratio | 50+ Wash Cycles | Eco-Fashion, Boutique Apparel |
| Discharge Printing | 100% Dark Cotton Knits | Zero-Feel (In-Fiber Dye) | 95% Match Ratio | Lifetime Garment Wash | Luxury Streetwear & Heavy Tops |
| High-Density Plastisol | Cotton/Poly Blends, Fleece | Structured / Opaque | 100% Exact Pantone | 60+ Wash Cycles | Band Merch, Heavyweight Hoodies |
| 3D Puff Printing | Heavyweight French Terry, Canvas | Raised 3D Texture | 92% Match Ratio | 40+ Delicate Washes | Bespoke Streetwear Typography |
| Silicone Screen Print | Spandex, Nylon Activewear | High Elasticity / Smooth | 96% Match Ratio | 75+ Performance Washes | Gymwear, Leggings, Athletic Gear |
End-to-End Custom Apparel Manufacturing: From Tech Pack to Bulk Shipping
Many UK apparel start-ups and retail buyers encounter severe operational friction because traditional screen printers act solely as basic "decoration shops." If a blank t-shirt has poor seam stitching, erratic sizing, or excessive fabric shrinkage, even the finest screen print cannot save the final retail product. Our factory model solves this bottleneck through integrated Full Package Cut & Sew Manufacturing.
When you partner with our production network, your order moves through an engineered 8-step industrial process designed to eliminate variance and guarantee on-time delivery into UK fulfillment warehouses or direct-to-consumer retail centers:
Consultation & Tech Pack Analysis
We evaluate vector artwork files, Pantone shade codes, print placements, garment measurement charts, and target target costings to establish accurate project scope.
CAD Mockups & Pattern Drafting
Digital pattern makers translate flat sketches into graded technical CAD specifications, calculating shrinkage rates and print coordinates for exact proportion matching.
Bespoke Fabric Sourcing
We source certified combed ring-spun cotton, GOTS-certified organic knits, heavyweight fleece (380-500 GSM), and technical stretch polyesters tailored to your exact hand-feel requirements.
Prototyping & Pre-Production Sample
A physical sample is constructed, screen printed, and private labeled. Sent directly to your UK office for fit testing, color review, and sign-off before full cutting.
Precision Automated Cutting & Sewing
Fabric rolls are relaxed, laser-cut to eliminate edge warping, and assembled by specialized seamstresses using reinforced flatlock or twin-needle stitching machines.
Automated Screen Printing & Curing
Garment panels are loaded onto high-speed automatic carousel printing presses. Inks are precisely squeegeed, flash-cured, and passed through gas-fired industrial drying tunnels.
AQL 2.5 Quality Assurance
Inspectors review print registration, ink cure depth, seam elasticity, thread trimming, and dimensional stability. Any non-conforming piece is rejected instantly.
Private Labeling & UK Fulfillment
Custom woven neck tags are attached, swing tags affixed, and garments neatly poly-bagged and boxed with tracked courier delivery straight to UK destinations.
Localized UK Application Scenarios & Regional Market Dynamics
The UK apparel market is distinctly diverse, driven by unique regional consumer expectations and stringent quality benchmarks. Working with a dedicated screen printing and garment factory allows UK businesses to tailor product development specifically to regional market trends:
1. London & Urban Streetwear Fashion Labels
Independent fashion brands operating out of creative hubs like East London (Shoreditch, Hackney, Soho) require vintage washed aesthetic treatments, heavy-duty boxy fit t-shirts (240+ GSM), and oversized heavyweight hoodies (450 GSM French Terry). Screen printing preferences skew heavily toward distressed discharge prints, subtle tonal high-density branding, and neck-tag replacement with custom woven satin labels. Our manufacturing ecosystem excels in producing these high-end, short-run streetwear drops with quick restock turnarounds.
2. Corporate Merch & Tech Sector in Cambridge, Oxford, & London City
Corporate clients, high-growth financial technology firms, and university institutions require bulk polo shirts, executive crewnecks, premium organic socks, and eco-friendly tote bags. The primary focus here centers on carbon footprint reduction, OEKO-TEX Standard 100 compliance, and color consistency across multiple re-orders. Our GOTS-certified water-based screen printing ensures zero chemical off-gassing and clean eco-credentials for UK corporate sustainability reporting.
3. Sustainable Activewear & Fitness Brands in Manchester & Northern Hubs
Manchester’s historic textile legacy lives on through modern athleisure and activewear brands. Technical running socks, high-waisted compression leggings, and sweat-wicking training tees demand stretch-resistant screen printing. Utilizing specialized multi-component silicone inks, our factories create reflective safety branding and dynamic elastic logos that retain structural integrity during high-intensity athletic training.
Key Advantages: Manufacturing Partner vs. Overseas Importers
Navigating post-Brexit customs procedures, import tariffs, and volatile international shipping costs has made direct overseas sourcing increasingly complex for UK business owners. Collaborating with an integrated production model offers distinct operational benefits:
- Zero Unexpected UK Import Tariffs: Clean export documentation and transparent shipping logistics eliminate surprise customs holds or unexpected VAT bills at the border.
- Low MOQ Flexibility (50–100 Pieces): Test new seasonal designs or limited-edition drops without locking capital in excess inventory. Scale smoothly into thousands of units as sales data validates demand.
- Exact Color Consistency via Pantone Matching: We utilize digital spectrophotometers to guarantee that your brand’s signature hue matches perfectly across screen printed apparel, embroidered caps, and custom knitted socks.
- Rapid Sampling Cycle (20-25 Business Days): Rapid physical prototyping allows UK buyers to physically hold, wear-test, and refine garments prior to authorizing bulk production runs.
Unregulated Overseas Factory Risks
- Extremely high MOQs (500-1000+ pieces per style required)
- Inconsistent ink curing resulting in print peeling after 2-3 washes
- Unpredictable shipping delays, port customs seizures, and extra fees
- Unvetted fabric sourcing leading to severe garment shrinkage
- No recourse for misprinted orders or damaged shipments
Our UK-Optimized Factory Solution
- Low MOQs starting at 50-100 pcs: Protect cash flow while scaling
- Industrial Curing & Wash Testing: Guaranteed 50+ wash durability
- Seamless Delivery & Customs Support: Full tracking to your UK door
- Pre-Shrunk Premium Textiles: GSM verified combed cottons
- Dedicated Account Management: Technical support at every stage
UK Screen Printing & Factory FAQ
Get instant clarity on minimums, turnarounds, pricing factors, and technical specifications for custom UK production orders.
What is the minimum order quantity (MOQ) for custom screen printed apparel in the UK?
Our minimum order quantities start at 50 to 100 pieces per style/design. Unlike rigid overseas factories that demand 500+ units, our flexible floor planning allows emerging UK clothing brands, independent labels, and corporate clients to produce small batch collections without excessive initial inventory risk.
How long does physical sampling and bulk production take for UK orders?
Physical pre-production sampling generally takes 20 to 25 business days from final vector artwork approval. Once you review and sign off on the sample fit, finish, and print quality, full bulk production takes 25 to 30 business days, followed by fast, tracked courier delivery straight to your specified UK address.
Can you provide complete private labeling, custom neck tags, and branded packaging?
Yes. We specialize in full-package private label manufacturing. We can remove generic manufacturer tags and install custom woven neck labels, screen printed size tags, custom branded hangtags, barcode stickers, and custom poly bags so your garments arrive 100% retail-ready for immediate sales or UK 3PL fulfillment.
What artwork files do you require to ensure accurate screen print rendering?
We require vector files created in Adobe Illustrator (.AI, .EPS, or print-ready vector .PDF) with all text outlines expanded. Color codes should be specified using the Pantone Matching System (PMS Solid Coated). If you only possess raster imagery (.PNG or .PSD), our graphics team can vectorize and separate channels for screen production.
Which fabrics and garment types can be manufactured and screen printed?
We work across a vast spectrum of raw textiles including 100% ring-spun combed cotton, GOTS-certified organic cotton, French terry fleece (300-500 GSM), polyester performance mesh, viscose, elastane blends, and custom knitted accessories such as jacquard socks, hoodies, t-shirts, sweatshirts, tracksuits, activewear, and caps.
How do you guarantee that prints will not crack, fade, or peel after washing?
Wash durability depends on correct ink curing chemistry. We cure every garment through industrial gas conveyor dryers calibrated to exact dwell times and temperatures (160°C/320°F). Additionally, our pre-production quality inspection team performs standardized wash-stretch tests (AATCC standards) to guarantee 50+ wash longevity without degradation.