Low MOQ
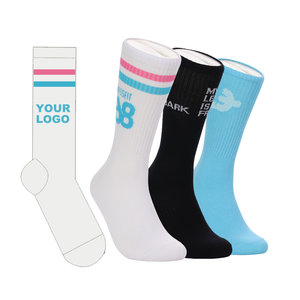
Engineered with premium combed cotton, high-density gauge counts, anti-blister padding, and eco-certified yarn matrices for retail brands worldwide.
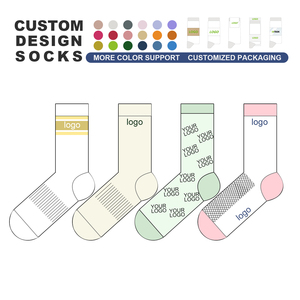
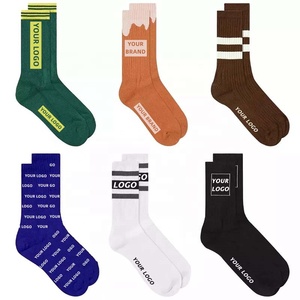
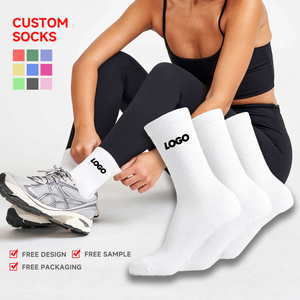
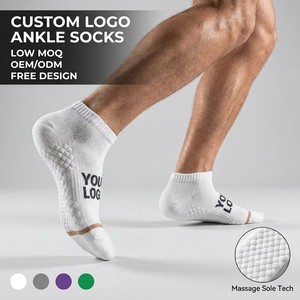
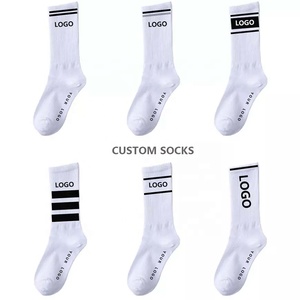
Strategic Sourcing Insight: In modern apparel supply chains, private label success hinges on reducing Time-to-Market (TTM) while guaranteeing AQL 2.5 Quality Compliance. By integrating full-package cut-and-sew, 200-needle circular knitting, and in-house embroidery under one unified standard, enterprise buyers achieve up to 35% lower landed costs and zero inventory friction.
Combining decade-long manufacturing expertise with state-of-the-art facility infrastructure in Charlotte, NC and Los Angeles, CA.
Complete control over pattern drafting, 3D CAD modeling, fabric nesting, and automated laser cutting. We transform raw textiles into retail-ready apparel with absolute dimension consistency.
Seamless brand transformation with high-density woven neck tags, eco-friendly heat transfer care labels, customized hangtags, and branded polybag packaging.
Multi-stage quality checks based on international AQL 2.5 standards. Every production run undergoes pre-shrinkage washing, seam tensile testing, and print durability validation.
A comprehensive analysis of global garment procurement, eco-textile innovations, and technical manufacturing benchmarks for enterprise buyers.
| Manufacturing Parameter | Standard Commercial Grade | Our Premium Private Label Benchmark | Commercial Value Advantage |
|---|---|---|---|
| Yarn Grade & Fiber Purity | Carded Cotton (20s-24s Count) | Long-Staple Combed Cotton (32s-40s Count) | +40% Tensile Strength, Ultra-Soft Feel |
| Knitting Gauge / Machine Specs | 144 Needle Standard Circular Knit | 168N to 200N High-Density Italian Machines | Higher Artwork Clarity & Elastic Recovery |
| Toe Closing Technology | Traditional Machine Overlock Loop | Hand-Linked Seamless Rosso / Rosso-Auto | Zero Friction Toe Seam, Anti-Blister Comfort |
| Functional Finishing | Basic Silicone Softener | SILVADUR™ Anti-Microbial + Moisture-Wick | 99.9% Bacteria Suppression up to 50 Washes |
| Eco-Compliance Standard | Uncertified Conventional Dyes | OEKO-TEX Standard 100 & GOTS Organic Certified | REACH Compliant for EU & US Retail Markets |
Traditional apparel supply chains locked buyers into 3,000+ unit minimums per colorway, binding substantial capital in slow-moving stock. Modern sourcing models demand flexible, low-MOQ runs (50 to 100 units per style) paired with rapid replenishment capability.
By leveraging digital CAD marker nesting and agile modular sewing lines, private label brands can test diverse market segments without inventory exposure, scaling production dynamically based on real-time sell-through telemetry.
Procurement strategies have shifted dramatically toward technical performance blends. In activewear and functional hosiery, the strategic combination of long-staple combed cotton with moisture-wicking synthetic channels (such as Coolmax or Supplex) creates micro-climate thermal regulation.
Furthermore, integrating elastane fibers directly into the core yarn (Core-Spun Technology) prevents sag over extended usage, retaining structural compression across 100+ wear cycles.
Global consumer demand and regulatory frameworks (including the EU Digital Product Passport) mandate transparency from raw fiber sourcing to final packaging. Enterprise suppliers must furnish verifiable certification across the product lifecycle.
Our facility incorporates GOTS-certified organic cotton, recycled PET polyester (rePREVE®), non-toxic Oeko-Tex dyes, and 100% biodegradable cornstarch polybags, protecting brand equity in environmentally conscious markets.
How an order transitions from technical drawing to fully audited, packaged retail cartons.
Evaluation of garment specifications, design target, target GSM weight, yarn blend, and delivery schedule.
Precision digitizing of tech packs, vector alignment, point-of-measurement (POM) sizing table construction.
Color lab-dip matching (Pantone TPX/TCX), yarn lot verification, and pre-production fabric GSM testing.
Physical sample creation in base size for fit assessment, stretch recovery, and client sign-off.
Computerized 200N circular knitting or automated cut-and-sew line assembly following approved CAD specs.
Application of high-density embroidery, screen printing, jacquard weaving, or heat-transfer brand tags.
Dimensional measurement verification, needle detection scan, seam pull-strength, and wash fastness audit.
Individual polybag sealing, inner carton packing, barcode labeling, and tracked international freight shipment.
Key information regarding minimum order thresholds, sampling timelines, custom branding capabilities, and global logistics.
Our minimum order quantity starts flexibly at 50 to 100 pieces per style/colorway depending on garment complexity. For standard circular knit hosiery and basic tees, 50 pieces is fully accessible. Custom dyed yarns or specialized performance fabrics may require higher thresholds based on mill batch minimums.
Prototyping and sample development typically take 7 to 10 business days after artwork and tech pack approval. Bulk production requires 20 to 25 business days depending on order volume, embellishment complexity, and raw material availability. Expedited production slots are available for high-priority drops.
To provide a firm, itemized quote, our engineering team requires five core specifications: (1) Fabric composition & GSM weight, (2) Detailed tech pack or reference sketch with measurements, (3) Color references (Pantone codes), (4) Desired artwork application (embroidery, Jacquard, screen print), and (5) Quantity breakdown per size.
Yes, we deliver 100% retail-ready apparel. Our private label finishing includes woven neck tags, printed size/care labels, custom branded hangtags with safety pins, barcode stickers, individual protective polybags, and custom printed shipping boxes ready for direct 3PL fulfillment.
We match colors directly against Pantone Fashion, Home + Interiors (TPX/TCX) standards via automated spectro-photometer testing. Fabric quality is verified using GSM weight scales, shrink-testing pre-wash chambers, and AQL 2.5 visual and structural inspection before goods are cleared for packing.
We accommodate EXW, FOB, CIF, and DDP (Delivered Duty Paid) shipping. We partner with top-tier international freight carriers (DHL, FedEx, UPS, and ocean freight partners) to manage customs clearance, export paperwork, and door-to-door tracking for clients across North America, Europe, Australia, and Asia.
Absolutely. We manufacture high-performance athletic wear equipped with moisture-wicking properties, 4-way elastic stretch, graduated compression zones, anti-odor silver-ion finishing, flatlock non-chafing seams, and mesh ventilation panels engineered for elite sport performance.
We adhere to strict confidentiality protocols. Prior to receiving your tech packs or custom artwork, we execute binding Non-Disclosure Agreements (NDAs). Your proprietary patterns, logos, and custom molds are reserved exclusively for your production lines and are never re-used or resold.
Partner with a top-trusted apparel manufacturer. Submit your design specifications or connect with our product engineering team today for an accurate quote and fabric sample kit.