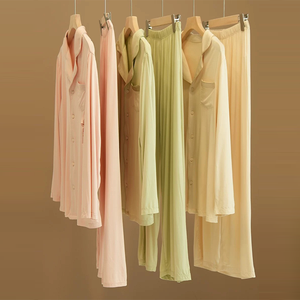
Catalog Showcase
Featured Custom Loungewear & Sleepwear Lines
Explore our benchmark private label loungewear collections engineered for global fashion brands, e-commerce retailers, and boutique labels.
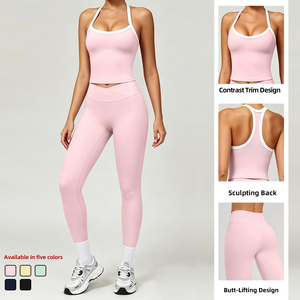
ABX6001+ACK6001 Custom Solid Women Loungewear Set Quick Dry Sports Workout Yoga Set High Stretch Gym Set
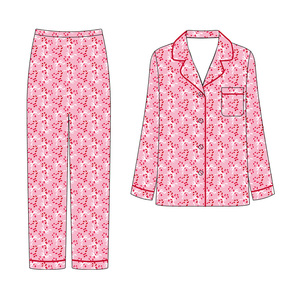
Custom Loungewear Women Sets Pajama Set 2 Piece Premium Cotton Women's Sleepwear Lounge Wear Sets
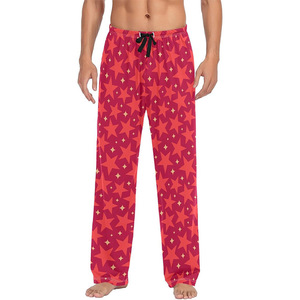
Wholesale Custom Logo Men Pajama Premium Long Pants Plus Size Drawstring Closure Sleepwear Loungewear Pjs
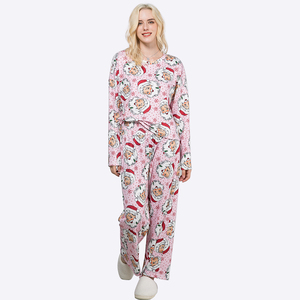
Custom Loungewear Manufacturer Women's Sleepwear Pajamas Set Lounge Wear Shirt Pants Two-Piece Set
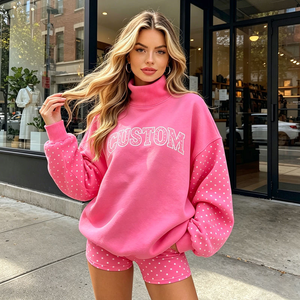
Custom Polka Dot Printed Patchwork Mockneck Cozy Sweatshirt Casual Short Set Drop Shoulder Loungewear
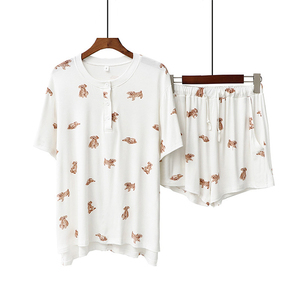
Custom Print Summer Knitted Modal Women Loungewear Sets Breathable Lightweight Pajamas
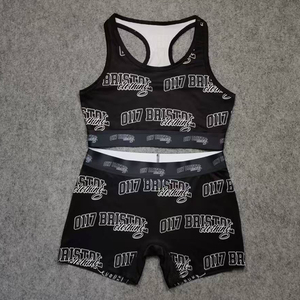
New Style Custom Polyester Knit Women's 2 Piece Set Leggings and Short Sleeve Top Casual Loungewear
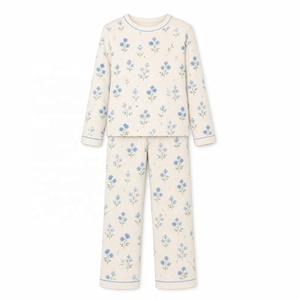
Custom Printed 93% Bamboo Viscose 7% Spandex Women Floral Loungewear Set Breathable Long Sleeve Pjs
Industry Whitepaper
The B2B Strategic Sourcing Guide for Custom Loungewear Manufacturing in China
Navigating technical fabric selection, low-MOQ cut-and-sew operations, OEM/ODM quality control standards, and sustainable supply chain scalability.
The global loungewear and sleepwear market has experienced a permanent structural shift. What was once classified as basic, low-margin nightwear has evolved into high-performance, aesthetically elevated "Sleep-to-Street" hybrid apparel. Today's consumer demands buttery-soft hand feel, structural garment durability, breathability, and non-toxic, eco-certified textiles. For growing fashion brands, DTC labels, and wholesale distributors, sourcing custom loungewear from established Chinese manufacturing hubs presents an unparalleled opportunity to balance high gross margins with premium build quality.
However, selecting the right apparel production partner requires moving beyond simple price-per-unit quotes. Sourcing executives and fashion entrepreneurs must evaluate fabric GSM consistency, tech pack translation fidelity, seam construction engineering, and factory compliance certifications. This whitepaper provides a comprehensive roadmap for partnering with China’s premier custom loungewear manufacturers, detailing fabric innovation, supply chain management, low minimum order quantity (MOQ) strategies, and quality assurance protocols.
50–100
Flexible Starting MOQ
93%
Bamboo Viscose Yield
20–25
Days Sampling Lead Time
AQL 2.5
Global QC Benchmark
Information Gain Insight: Unlike standard promotional apparel manufacturers, specialized loungewear factories utilize 4-needle 6-thread flatlock stitching and bio-wash enzymatic finishing to eliminate interior seam chafing and guarantee less than 3% post-wash dimensional shrinkage.
1. Emerging Sourcing Trends & Future Market Outlook (2025–2030)
To maintain market share in a crowded apparel landscape, brand owners must align their product development with global consumer shifts. The loungewear industry is undergoing four major technical and operational revolutions:
Eco-Luxury & Bio-Based Fibers
Synthetic polyesters are rapidly being replaced by bio-based knits. Micro-Modal derived from beechwood pulp, GOTS-certified organic combed cotton, and high-density 93% Bamboo Viscose blends with 7% Elastane now dominate premium pyjama lines due to their natural thermoregulation and hypoallergenic properties.
Agile Low-MOQ Production
The traditional requirement of 1,000 to 3,000 units per style forced brands into inventory over-accumulation. Modern Chinese garment factories utilize digital CAD pattern grading and flexible modular sewing lines, allowing brands to launch initial drops at 50 to 100 pieces per colorway while preserving bulk margin economics during replenishment reorders.
Full Technical Package Precision
Precision engineering is essential. Professional loungewear suppliers work directly from comprehensive Tech Packs specifying precise stitch-per-inch (SPI) ratios, seam elasticity thresholds, reactive dye pantone formulas, and customized zero-plastic eco-packaging specs.
Non-Toxic OEKO-TEX Standard 100 Dyes
Because sleepwear remains in direct contact with skin during sleep, compliance with global toxicological safety standards is non-negotiable. Modern factories enforce strict eco-friendly dye controls to guarantee zero formaldehyde, heavy metals, or hazardous azo compounds.
2. Technical Fabric Sourcing & Specification Benchmark Matrix
Selecting the optimal fabric blend is the single most critical factor determining product rating, return rates, and customer lifetime value. Below is an engineering comparison matrix of primary loungewear textiles utilized in premier custom manufacturing:
| Fabric Composition | Optimal GSM Range | Breathability Index | Shrinkage Rate | Eco-Certification | Primary Product Application |
|---|---|---|---|---|---|
| 93% Bamboo Viscose / 7% Spandex | 180 – 220 GSM | Very High (9.8/10) | < 2.5% (Pre-Shrunk) | OEKO-TEX / FSC | Luxury Button-Down Pajama Sets, Soft Robes |
| 100% Micro-Modal Knit | 170 – 200 GSM | Ultra High (9.9/10) | < 3.0% | TENCEL™ Certified | Lightweight Summer Loungewear, Camisoles |
| GOTS Organic Combed Cotton | 220 – 280 GSM | High (8.5/10) | < 2.0% | GOTS / Organic 100 | Classic Lounge Tops, Relaxed Drawstring Pants |
| Cotton French Terry / Fleece | 300 – 380 GSM | Moderate (7.2/10) | < 2.0% | BCI Cotton | Cozy Mockneck Sweatshirts, Casual Shorts Sets |
| Poly-Spandex Athletic Knit | 240 – 300 GSM | Moisture-Wicking | < 1.0% | GRS Recycled Poly | Active Yoga Sets, High-Stretch Fitness Loungewear |
3. Enterprise Manufacturing Capabilities & OEM/ODM Advantage
Our custom garment manufacturing operations are built specifically to bridge the gap between small-batch boutique startups and multi-national apparel brands. By maintaining direct control over fabric milling, pattern engineering, cut-and-sew operations, and retail-ready packaging, we provide an integrated end-to-end solution.
Integrated Cut & Sew Precision
Unlike standard off-the-shelf print-on-demand dropshippers, true custom manufacturing begins with raw fabric rolls. Our cutting rooms utilize automated laser-guided cutting tables to guarantee pattern piece consistency across all size runs (XS to 5XL). Every seam—from reinforced side slits to elastic waistband encasements—is constructed using high-tensile threads to prevent seam popping after wash cycles.
Private Label & Retail Branding Solutions
We provide full white-glove private labeling services to ensure your garments arrive ready for immediate warehouse intake or direct-to-consumer fulfillment:
- Custom Neck Labels: High-density woven tags, ultra-soft printed satin labels, or tagless heat-transfer neck prints for irritation-free necklines.
- Custom Trims & Hardware: Engraved mother-of-pearl buttons, custom branded metal aglets, embossed drawcords, and custom woven waistbands.
- Retail Packaging: Biodegradable frosted poly bags with custom scannable barcodes, custom hangtags, branded tissue paper, and unboxing mailer boxes.
4. The 8-Stage OEM/ODM Production Workflow
Every custom loungewear order undergoes a rigorous 8-stage manufacturing process designed to enforce complete transparency and eliminate defect risks before bulk shipping.
01
Tech Pack & Consultation
We review your sketches, size charts, fabric preferences, and order quantities to establish exact pricing and lead times.
02
CAD Pattern & Mockups
Our master patternmakers convert your design into digital vector CAD patterns with precise point-to-point measurement specs.
03
Fabric Sourcing & Dyeing
Yarns are milled, custom lab-dips are dyed to match Pantone standards, and GSM density tests are verified.
04
Prototyping & Sampling
A physical sample is cut, stitched, and delivered to your office for real-world fit, stretch, and wash testing.
05
Precision Bulk Cutting
Upon sample approval, graded pattern markers are executed across automated cutting lines for zero fabric waste.
06
Sewing & Customization
Expert seamstresses assemble garments using flatlock or coverstitch lines, applying screen prints or custom embroidery.
07
AQL 2.5 Quality Inspection
Dedicated QC inspectors verify seam strength, measurements, loose threads, print cure, and button attachment stability.
08
Packaging & Freight
Garments are ironed, poly-bagged, barcoded, and packed into heavy-duty cartons for door-to-door tracked freight shipment.
5. Frequently Asked Sourcing & Procurement Questions (FAQ)
Address common manufacturing and supply chain queries to streamline your procurement process:
What is your minimum order quantity (MOQ) for custom loungewear?
Our flexible low-MOQ production starts at 50 to 100 pieces per style/colorway for standard knitted fabrics like modal, cotton, and polyester blends. For specialized custom-milled jacquards or custom yarn-dyed plaid fabrics, MOQs range from 200 to 300 pieces due to dye-house minimum batch requirements.
Can you manufacture loungewear without a pre-existing technical pack?
Yes! If you do not have a formal vector Tech Pack, you can send us physical sample garments, reference photos, or rough design sketches along with desired dimensions. Our in-house technical design team will reverse-engineer the pattern and draft a comprehensive factory-ready spec sheet for your approval.
What are the standard sampling and bulk production turnaround times?
Physical fit sample creation typically takes 15 to 20 business days after design confirmation. Bulk production takes approximately 25 to 30 business days following final sample sign-off, depending on total volume, decoration complexity, and fabric lead times.
How do you guarantee color consistency and prevent post-wash shrinkage?
All fabric batches undergo lab-dip color matching against Pantone TCX/TPG color codes and undergo pre-shrinking bio-wash steaming prior to cutting. This ensures strict color batch uniformity and keeps post-wash dimensional shrinkage under 3% across all standard washing cycles.
Do you manage international shipping, customs clearance, and duties?
Yes, we provide global logistics support including Express Air Freight (DHL/FedEx/UPS 5-7 days), Air Cargo DDP, and Ocean Freight DDP (Delivered Duty Paid). We handle all export/import customs paperwork so goods arrive directly at your warehouse or fulfillment center without unexpected fees.