Enterprise Product Recommendations & Private Label Manufacturing
Direct factory apparel solutions engineered with low MOQs, high tensile durability, and full custom branding integration.
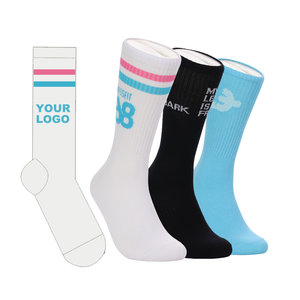
Custom Socks Factory No Minimum Order High Quality Cotton White Socks
Premium combed cotton construction featuring high-density logo embroidery, seamless toe closing, and reinforced cushion heel support.
Contact Us
Personalized Logo Embroidered Men Crew Fashion & Dress Socks
Custom knit jacquard dress socks engineered with 200-needle fine gauge structure, elastane stretch recovery, and branded packaging options.
Contact Us
Unisex Jacquard Logo Crew Socks Low MOQ Flexible Batching
Direct-to-garment and jacquard pattern capabilities designed for boutique apparel labels requiring small batch production runs.
Contact Us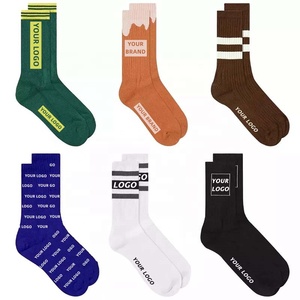
Designer Jacquard Knitted Anti-Bacterial Heavy Duty Sport Socks
Heavyweight 100% combed cotton yarn treated with anti-bacterial silver ion finishes and high-impact letter bottom knitting.
Contact Us
Personalized Gym Crew Athletic Socks for Activewear Labels
Moisture-wicking athletic knit with targeted arch support compression and precision embroidery branding for fitness brands.
Contact Us
Breathable Performance Sports Basketball & Running Socks
Technical multi-channel synthetic yarn engineered for high ventilation, thermal regulation, and anti-blister friction reduction.
Contact Us
Custom Logo Anti-Blister Massage Ankle Socks & Luxury Hospitality
Low-cut ergonomic design featuring silicone massage grip sole patterns and ultra-soft organic cotton fibers for luxury resort amenities.
Contact Us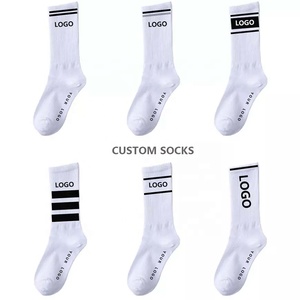
OEM Fast-Track Athletic Cycling & Basketball Crew Socks
Rapid prototyping OEM product line supporting custom color dyes, dynamic compression zones, and fast 20-day turnaround schedules.
Contact UsExecutive Summary: Top 10 Custom Denim Exporter Benchmarks & Sourcing Intelligence
The global denim export market is undergoing a seismic paradigm shift driven by technological automation, eco-compliant finishing standards, and hyper-agile supply chain architecture. For international retail brands, luxury streetwear labels, and commercial wholesalers, identifying elite manufacturing partners requires looking beyond superficial pricing metrics to evaluate core technical competencies: warp-and-weft tensile resilience, indigo rope-dye consistency, elastane retention curves, and automated pattern grading accuracy.
As leading custom denim exporters, modern facilities must combine traditional artisan craft with industry 4.0 automation. Sourcing managers navigating the global market encounter substantial variance in fabric weights (ranging from lightweight 8 oz summer denims to heavy 14.5 oz selvage formulations), wash wash-fastness certifications, and sustainable laser distressing capabilities. Selecting an exporter equipped with integrated OEM/ODM capabilities guarantees that tech packs are executed with millimeter-level fidelity.
Our integrated manufacturing floor operates on a full-package protocol. Whether you are scaling an established private label or launching a specialized capsule collection, our factory infrastructure provides a seamless pathway from raw fiber selection to store-ready shelf delivery. By unifying custom denim manufacturing with specialized knitted apparel lines—such as performance socks, fleece hoodies, and cut-and-sew separates—brands achieve structural freight efficiency and unified quality control under a single corporate point of contact.
Export Manufacturing Standards: Technical Benchmark Matrix
Understanding the operational parameters of elite denim exporters enables procurement executives to mitigate risk, audit supply chains, and secure optimal gross margins.
| Evaluation Parameter | Standard OEM Exporters | Tier-1 Enterprise Custom Exporters | Value Delivered to Brand |
|---|---|---|---|
| Minimum Order Quantity (MOQ) | 500 – 1,000 Pcs / Style | 50 – 100 Pcs / Style (Flexible) | Eliminates deadstock inventory & frees working capital |
| Wash & Finish Capabilities | Basic Chemical Stone Wash | Ozone Wash, Laser Abrasion, Enzymatic Eco-Wash | Authentic vintage aesthetics with eco-certification compliance |
| Pattern & Fitting Accuracy | Manual Cut & Paper Templates | 3D CAD Patterning & Automated Laser Cutting | Zero size variance across batch production runs |
| Quality Assurance Standard | End-of-line spot checks | AQL 2.5 / 4.0 Multi-stage Inline Inspection | Sub-0.5% defect return rates for retail distribution |
| Turnaround & Sampling | 45–60 Business Days | 20–25 Days Sample / 25–30 Days Bulk | Faster time-to-market for seasonal releases |
Enterprise Advantages: Why Global Brands Partner With Us
Building a successful private label apparel brand requires an export partner capable of resolving the key tension of modern apparel retail: balancing low minimum production volumes with strict industrial quality standards. Our global operations, backed by key logistics and management hubs in Charlotte, NC and Los Angeles, CA, combine localized communication with cost-effective international production lines.
Low MOQ Production Planning
We structure our cutting tables specifically to accommodate runs starting at 50 to 100 units per style. Test new denim washes, fit profiles, or custom knitted lines without locking up capital in unproven inventory.
Comprehensive Quality Control
Every garment undergoes rigorous multi-point inspections covering GSM weight verification, seam pull tension tests, dimensional wash-shrinkage analysis, and precise trim and print alignment before boxing.
End-to-End Private Labeling
Transform raw garments into complete retail-ready collections with custom woven neck labels, printed care tags, custom die-cut hangtags, barcoded poly bags, and branded shipper boxes.
Future Sourcing & Procurement Trends in Custom Denim Export (2025–2030)
Navigating the next decade of denim procurement requires alignment with global regulatory directives, changing consumer sustainability standards, and technological advances in textile manufacturing. Brands that fail to integrate these strategic shifts risk supply chain disruption and declining brand equity.
1. Closed-Loop Circular Fiber Integration: The global transition toward circular textiles has shifted post-consumer recycled cotton (PCC) and organic GOTS-certified fibers from niche options to commercial imperatives. Advanced denim exporters now incorporate up to 30% recycled cotton content into warp yarns without sacrificing tensile strength or abrasion longevity.
2. Waterless Eco-Finishing Technologies: Water usage in traditional garment processing is facing strict international regulatory limits. Modern export facilities utilize micro-bubble technology, nebulization, and ozone processing to achieve classic indigo distress levels while reducing fluid waste and eliminating harmful chemicals like potassium permanganate.
3. AI-Driven Tech Pack Digitization & 3D Prototyping: Virtual sampling is revolutionizing sample development cycles. By utilizing 3D garment simulation tools, custom denim manufacturers create digital twin samples that accurately model drape, stretch, and stress patterns, cutting physical sample iterations by over 50% and accelerating production timelines.
4. Nearshoring Supply Chains & Dual-Hub Freight Routing: Geopolitical complexity has highlighted the vulnerability of single-source production routes. Modern export strategies combine overseas cost efficiencies with domestic distribution hubs in key consumer markets, ensuring customs clearance proceeds without supply chain bottlenecks.
Industry Development Trends: Technical Fabrics & Custom Apparel Synergy
The boundaries defining traditional denim apparel, technical sportswear, and luxury casualwear continue to blur. Consumer preference has tilted toward high-performance hybrid garments that offer structural durability alongside ergonomic stretch and moisture management.
Leading exporters are responding by weaving high-tenacity elastane blends (such as Lycra DualFX technology) into premium denim weaves, preventing structural bagging at knees and waistlines over extended wear. Simultaneously, this technical approach extends to custom knitted items—such as high-density performance socks, heavy French terry fleece streetwear, and technical athletic wear—enabling unified collection drops with matching brand aesthetics.