Featured Custom Hosiery Lineup
Engineered with high needle counts, reinforced heel & toe construction, and customizable branding options.
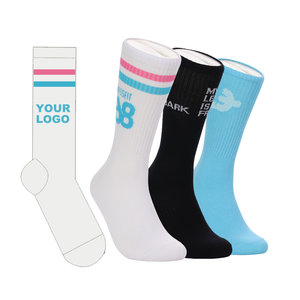
Custom Socks Factory Custom No Minimum Order High Quality Cotton White Socks Custom Socks With logo
Get a Quote
Unisex Crew Personalized Design Your Own Logo Sock Customized Socks Jacquard Custom Logo Socks Low MOQ
Get a Quote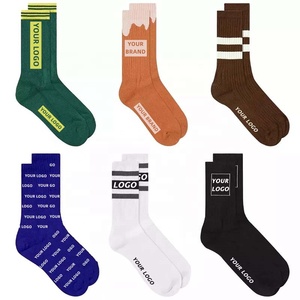
Designer Jacquard Knitted Crew 100% Cotton Thick Anti-Bacterial Brands Socks Casual Letter Bottom Logo
Get a Quote
Breathable Sports Basketball Crew Men Socks Custom Socks Logo Sport Socks Running Athletic Line
Get a Quote
Custom Design Cotton Socken Personalized Logo Embroidered Men Tube Fashion Socks Sox Crew Dress Socks
Get a Quote
Personalized White Letter Socks Custom Logo Gym Crew Socks for Women Embroidery Sport Athletic Cotton Socks
Get a Quote
Custom Logo Massage Ankle Socks Anti-Blister Cotton Breathable Low-Cut Luxury Gift Hotel Amenity
Get a Quote
OEM Fast Sample Custom Logo Crew Socks Men Running Sport Socks, Cycle Athletic Basketball Socks
Get a QuoteIndustrial OEM Engineering & Manufacturing Pillars
Modern sock manufacturing requires an intricate balance of fiber chemistry, precision circular knitting mechanics, and rigorous ergonomic design.
High Needle Gauge Density
We deploy advanced computerized Lonati circular knitting machinery across multiple needle counts to match exact design specs:
- 96N - 108N: Heavyweight outdoor, coarse terry boot socks.
- 144N - 168N: Standard athletic, ribbed street crew socks.
- 200N - 240N: High-definition dress socks, fine logo resolution, maximum elasticity retention.
Yarn Fiber Engineering
Premium tactile performance starts at the raw material level. Our yarn inventory covers sustainable and high-tech formulations:
- Long-Staple Combed Cotton: Zero pilling, smooth hand-feel.
- REPREVE® Recycled Polyester: Post-consumer eco-certified yarn.
- Coolmax® & Bamboo Viscose: Active moisture transport and natural antibacterial properties.
Precision Toe Seam & Fit Mechanics
Eliminating pressure points and friction standardizing zero-defect manufacturing:
- Hand-Linked (Rosso Seamless Toe): Completely flat toe closure avoiding blisters during prolonged wear.
- Y-Heel Pocket Construction: Anatomically contoured heel to prevent slipping.
- Graduated Compression Ribbing: Arch band support with targeted elastic tension.
1. The Evolution of OEM Sock Manufacturing: From Basic Commodity to Technical Footwear
In modern apparel supply chains, custom sock manufacturing has shifted dramatically from generic bulk commodity production to specialized, high-performance hosiery engineering. For global retail brands, corporate merchandising leaders, and private label startups, selecting the right OEM Custom Socks Manufacturer & Factory is the cornerstone of building product loyalty, minimizing return rates, and guaranteeing strong retail margins.
Traditional manufacturing setups relied on basic 120-needle machines using carded short-staple cotton, resulting in rapid fabric pilling, elasticity loss, and rigid toe seams that caused foot abrasion. Today, modern OEM factories utilize computerized double-cylinder and single-cylinder Italian Lonati machines running up to 200 to 240 needle counts. This technological leap allows factories to weave high-definition logos, micro-padded terry zones, and ergonomic arch supports directly into the fabric matrix without sacrificing stretchability or structural integrity.
2. Technical Needle Gauge Comparison for B2B Procurement
When issuing a Request for Quotation (RFQ) or building a Tech Pack for custom socks, understanding needle count (N) is crucial. Needle count determines the density of the knit, the intricacy of the artwork achievable via Jacquard weaving, and the thickness of the finished sock.
| Needle Count (N) | Ideal Product Application | Fabric Weight & Thickness | Artwork Capability |
|---|---|---|---|
| 96N - 108N | Heavy Work Boots, Winter Thermal, Outdoor Hiking Socks | Heavyweight / Ultra-Thick Terry | Bold, coarse patterns; basic blocks |
| 144N | Classic Athletic Crew, Retro Skate Socks, Thick Tube Socks | Medium-Heavyweight Cushion | Standard block logos, athletic stripes |
| 168N | Everyday Casual Streetwear, Gym & Fitness Socks | Medium Weight / Balanced Comfort | Detailed Jacquard text, moderate detail logos |
| 200N | Luxury Dress Socks, High-Performance Cycling & Running | Lightweight / High-Density Fine Knit | High-definition logos, micro-patterns, intricate text |
| 240N | Ultra-Thin Executive Dress Socks, Technical Compression Liner | Super Ultra-Light / Premium Silk-Feel | Micro-gauge precision detailing |
3. Material Composition & Yarn Science in Custom Hosiery
A sock's comfort, longevity, and functional properties are dictated by its raw material blend ratio. Professional custom sock manufacturers engineer yarn formulations according to end-user applications:
A. Combed Long-Staple Cotton (75% - 85%)
Unlike raw carded cotton, combed cotton undergoes an extra refining process that strips away short fibers and impurities. This produces an exceptionally smooth, soft yarn with high tensile strength that resists pilling after dozens of commercial wash cycles.
B. Synthetic Elastane & Lycra Core (12% - 20%)
To ensure high shape memory and prevent sagging around the calf, high-grade Spandex or original Dupont Lycra is wrapped with nylon threads. This core provides 360-degree cross-directional stretch, keeping crew socks locked in place during intense physical activity.
C. Functional Performance Yarns
- Coolmax® Polyester: Engineered with multi-channel cross-section fibers to pull moisture away from the skin toward the outer layer of the sock for rapid evaporation.
- Bamboo Viscose: Naturally hypo-allergenic and micro-porous, offering excellent thermal regulation and inherent odor reduction for luxury ankle and dress socks.
- Merino Wool: Nature’s premium technical fiber providing superior warmth-to-weight ratio, moisture vapor management, and flame resistance for rugged outdoor applications.
- Recycled Poly (GRS Certified): Made from post-industrial plastic bottles, allowing sustainable apparel brands to meet strict Scope 3 carbon reduction metrics.
4. Sourcing & Industry Trends for 2025 – 2030
As consumer preferences evolve toward functional activewear and environmentally responsible apparel, buyers and product managers should realign their procurement strategies with four macro trends:
Trend 1: Sustainable & Traceable Supply Chains
Retailers are shifting away from conventional virgin polyester. Leading global brands require OEM factories to hold certifications such as Global Recycled Standard (GRS), OEKO-TEX® Standard 100 (ensuring zero harmful chemical residues), and GOTS (Global Organic Textile Standard). Traceability from yarn spinning mill to packed carton is rapidly becoming a non-negotiable procurement requirement.
Trend 2: Bio-Functional & Anti-Blister Engineering
Modern consumers demand activewear socks that prevent sports injuries. Features such as 3D anatomical left/right foot beds, targeted midfoot arch compression bands, and friction-reducing seamless hand-linked toes are transitioning from niche athletic gear to mainstream streetwear collections.
Trend 3: Micro-Batch OEM Agility (Low MOQ Sourcing)
Holding excessive inventory poses significant cash flow risks. Leading OEM factories are restructuring production lines to support low Minimum Order Quantities (MOQs starting from 50 to 100 pairs per style/colorway). This enables ecommerce DTC brands to test fresh designs, validate market demand, and scale up bulk re-orders rapidly.
Trend 4: 360-Degree Seamless Digital Printing vs Jacquard Knitting
While traditional Jacquard weaving physically knits colored yarns together, 360° Seamless Digital Sublimation Printing injects eco-friendly dyes deep into polyester or bamboo fibers without leaving inner yarn floats. This technique allows complex photo-realistic graphics and gradient colorways without compromising sock stretch.
5. The 8-Stage OEM/ODM Quality Control Lifecycle
Our OEM factory protocol strictly adheres to the AQL 2.5 (Acceptable Quality Limit) standard, ensuring that every batch delivered to retail distribution centers meets rigorous international apparel specifications.
Stage 01: Tech Pack CAD Approval
Digitizing artwork, color matching with Pantone TCX codes, defining sizing grids and yarn gauge.
Stage 02: Yarn Inspection & Lab Dip
Testing raw cotton fiber length, color fastness, yarn elasticity tension, and dye lot consistency.
Stage 03: Prototyping & Sampling
Knitting initial physical samples for fit evaluation, dimensional verification, and stretch testing.
Stage 04: Computerized Circular Knitting
Precision automated production on Lonati machinery with continuous optical needle break monitoring.
Stage 05: Toe Linking & Seaming
Rosso auto-linking or hand-looping seamless toe closure depending on client tech specifications.
Stage 06: Boarding & Steam Setting
Thermal metal foot-form boarding to stabilize fabric dimensions, shape, and cross-directional stretch.
Stage 07: In-line & Final QC Inspection
Verifying sizing tolerance (±0.5cm), checking interior thread floats, seam pull testing, needle sweep inspection.
Stage 08: Retail Packaging & Logistics
Custom header cards, backer boards, polybagging, barcode labeling, and tracked export freight handling.
6. Why Global Apparel Brands Partner With Our Factory
Backed by over a decade of dedicated apparel manufacturing expertise, dual US administrative and logistics hubs (Charlotte, NC & Los Angeles, CA), and an extensive overseas factory floor footprint, we offer full turn-key manufacturing for growing labels and corporate enterprise accounts alike:
- Flexible Run Sizes: Scale seamlessly from initial small-batch market test runs (50-100 units/style) to high-volume bulk production runs exceeding 500,000 pairs.
- Full Private Label Customization: In-house production of custom woven neck/cuff labels, eco-friendly printed kraft header cards, custom metal clips, and retail-ready display boxes.
- Complete Tech Pack Support: No tech pack? Simply send us a physical sample garment or vector design sketch; our pattern engineering team will draft complete knitting schematics.
- Guaranteed Delivery Timelines: Locked calendar slots with predictable turnarounds—20 to 25 business days for sampling, and 25 to 30 business days for mass bulk production.
Frequently Asked Questions
Essential insights for purchasing managers, apparel designers, and supply chain directors.
What is the typical Minimum Order Quantity (MOQ) for custom OEM sock production?
Our minimum order quantity starts as low as 50 to 100 pairs per style/size/colorway for standard jacquard knitted crew and sport socks. For highly specialized technical yarns (such as custom-dyed Merino wool or specific high-compression gradient medical weaves), MOQs generally range from 300 to 500 pairs to cover yarn dye vat setups efficiently.
What file formats do you need to start sample production?
We accept vector graphic files including Adobe Illustrator (.AI), Scalable Vector Graphics (.SVG), or high-resolution PDF/EPS formats. Please specify Pantone (PMS TCX/TPG) color codes. If vector artwork is unavailable, our in-house design team can assist in creating scale CAD mockups from your image or sketch.
What is the difference between Rosso Linking and Hand-Linked Seamless Toes?
Rosso linking is an automated machine stitch that leaves a small, slightly elevated seam inside the toe cap—ideal for budget promotional or standard casual socks. Hand-linked (or seamless) toe closure manually loops every knit stitch together, creating an entirely flat seam that prevents rubbing and blisters, which is recommended for high-performance sports and luxury dress socks.
How long does the sample creation and bulk production cycle take?
Physical sample creation takes approximately 20 to 25 business days following CAD artwork approval and yarn selection. Bulk mass production requires 25 to 30 business days after the pre-production sample is physically signed off by your QA team.
Can you supply eco-friendly recycled yarn options with certified documentation?
Yes. We regularly manufacture using GRS-certified REPREVE® recycled polyester, GOTS-certified organic cotton, and FSC-certified bamboo viscose. Material transaction certificates (TC) can be provided with bulk shipments for full sustainability audit compliance.
How do you test and control color fastness and shrinkage during manufacturing?
All raw yarn lots undergo pre-knitting wash tests (ISO 105-C06 standard) to ensure a minimum color fastness rating of Grade 4. Finished sock samples undergo high-temperature boarding and steam-setting procedures, keeping dimensional post-wash shrinkage below 3%.
Do you provide complete retail-ready private label branding and packaging?
Absolutly. We engineer and produce full custom packaging including recyclable cardboard header cards, fold-over hangtags, custom UPC barcode stickers, self-adhesive branded polybags, and custom printed corrugated shipper boxes ready for direct 3PL fulfillment.
How are international customs duties, freight, and shipping handled?
We provide full DDP (Delivered Duty Paid), DAP, and FOB terms. Goods are dispatched with tracked air or ocean freight logistics partners, complete with HS tariff code classifications, commercial invoices, and certificate of origin documentation to prevent customs delays.
Ready to Start Production on Your Custom Sock Line?
Connect directly with our engineering and sales management team. Send your tech pack, sketch, or design requirements today to receive a comprehensive factory quotation and yarn sample kit.