Featured Custom Apparel & Sublimation Products
High-precision knitwear, athletic socks, and custom embroidered & sublimated textiles engineered for global brand compliance.
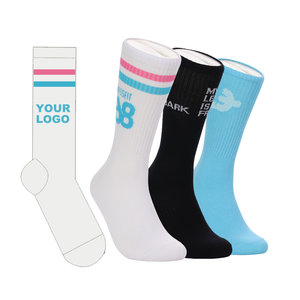
Custom White Cotton Socks Factory Low MOQ
- Material: 80% Combed Cotton / 17% Poly / 3% Spandex
- Craft: High-Density Knit + Precision Logo Embroidery
- Features: Reinforced Heel & Toe, Anti-Shrink
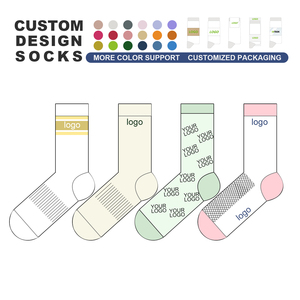
Personalized Embroidered Men Crew Tube Socks
- Needle Count: 168N / 200N Fine Gauge Stitching
- Design: Custom Jacquard & Side Embroidery
- Application: Casual Fashion, Streetwear Apparel
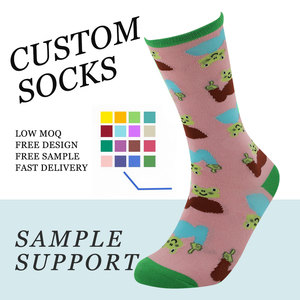
Unisex Custom Jacquard Logo Athletic Crew Socks
- Yarn Blend: Breathable Micro-Poly & Soft Cotton
- Color Match: Exact Pantone CMYK/PMS Calibration
- MOQ: Flexible Small Batch Starting at 100 Pairs
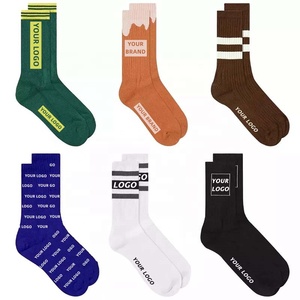
Thick Anti-Bacterial Knitted Designer Sports Socks
- Treatment: Silver-Ion Anti-Odor Technology
- Cushioning: Full Terry Cushion Sole Support
- Target: High-End Sportswear & Retail Brands
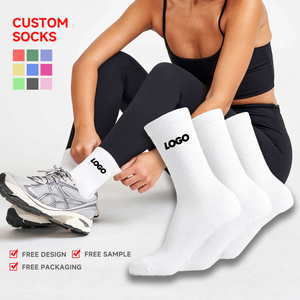
Women Athletic Gym Crew Socks with Custom Embroidery
- Arch Support: Ribbed Elastic Compression Band
- Finish: High-Fidelity Lettering & Sublimated Heel
- Durability: 50+ Industrial Wash Cycle Guarantee
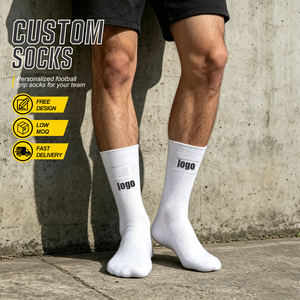
Breathable Performance Basketball & Running Socks
- Ventilation: Mesh Breathability Channels
- Printing: High-Resolution Dye-Sublimation Accents
- Fit: Ergonomic Left/Right Foot Anatomical Shape
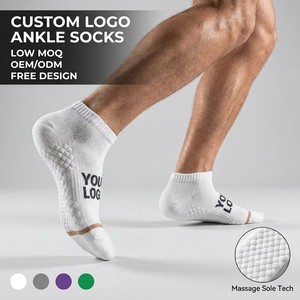
Luxury Anti-Blister Massage Ankle Gift Socks
- Sole Design: Tactile Anti-Slip Massage Nodes
- Packaging: Custom Retail Box & Branded Polybag
- Niche: Hotel Amenities, Spa & Luxury Merchandise
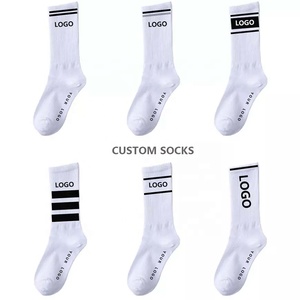
OEM Pro Cycling & Athletic Performance Socks
- Sublimation: 360-Degree Seamless Digital Transfer
- Lead Time: 3-Day Rapid Sampling & Express Shipping
- Certification: OEKO-TEX Standard 100 Certified Yarns
Technical Evaluation: The Engineering Behind China’s Dye-Sublimation Printing Leadership
In modern textile manufacturing, dye-sublimation printing represents the pinnacle of chemical engineering and thermal transfer physics. Unlike conventional screen printing—which deposits a layer of plastisol or water-based ink on top of fabric fibers—dye sublimation utilizes thermal energy to trigger a molecular transition. Under precise parameters of temperature (190°C to 215°C) and pressure (4.5 to 6 bar), disperse dye particles instantaneously sublime from a solid state into a gas without entering a liquid phase.
During this micro-second reaction, the synthetic polymers of polyester, micro-polyamide, or elastane blends expand, opening microscopic inter-molecular voids. The gaseous dye penetrates deep into the polymer core, bonding permanently with the synthetic filaments upon cooling. The result is an indelible, full-gamut chromatic finish that exhibits zero surface hand-feel, zero cracking, and uncompromised breathability across high-performance activewear, custom athletic socks, and promotional apparel.
As leading China sublimation printing suppliers and B2B exporters, our manufacturing facility leverages state-of-the-art Italian EFI Reggiani and Japanese Mimaki digital sublimation presses paired with Swiss-engineered Klieverik rotary calenders. This technical setup resolves historical industry bottlenecks, ensuring pitch-perfect color fidelity across continuous high-volume production drops.
Molecular Fiber Bonding vs. Surface Deposit Printing
To evaluate why enterprise global apparel brands are shifting purchase orders toward China’s advanced sublimation infrastructure, procurement officers must understand the mechanical and structural contrasts between print methodologies:
| Performance Metric | Dye-Sublimation Transfer | Direct-to-Garment (DTG) | Screen Printing (Plastisol) | Jacquard Knit Weaving |
|---|---|---|---|---|
| Color Gamut & Gradients | Unlimited (Photorealistic 1200 DPI) | High (CMYK + White) | Limited (Spot Colors) | Moderate (Yarn Count Bound) |
| Fabric Hand-Feel (Touch) | Zero Weight / Soft Touch | Soft to Moderate | Heavy / Rubberized Feel | Textured / Knitted Surface |
| Wash Fastness (ISO 105-C06) | Grade 4.5 - 5.0 (No Fade) | Grade 3.5 - 4.0 | Grade 3.0 - 4.0 (Cracks Over Time) | Grade 4.5 - 5.0 |
| Fabric Breathability | 100% Retained (Pores Unblocked) | 80% Retained | Reduced (Ink Blocks Micro-Mesh) | 100% Retained |
| Economical Run Size | 50 to 50,000+ Units (Low Setup) | 1 to 500 Units | 500 to 100,000+ Units | 300 to 10,000+ Pairs |
Future Procurement & Technological Trends in Sublimation Apparel (2025–2030)
The global sublimation printing market is projected to reach $15.4 billion by 2030, driven by rapid consumer demand for personalized athletic gear, high-density custom socks, corporate merchandise, and sustainable athleisure. Sourcing directors and private label apparel brands must align their supply chains with three key technical trends:
1. Recycled PET & Bio-Based Substrates
Global ESG mandates require transition to recycled polyester (rPET) derived from post-consumer water bottles. Advanced Chinese suppliers now offer GRS-certified (Global Recycled Standard) sublimation fabrics that accept disperse dye molecules with identical brilliance and color fastness as virgin polyester.
2. 360-Degree Seamless Sock Printing
Traditional flat-press sublimation causes unwanted white line side-seams on cylindrical garments like crew socks. Next-generation 360-degree roller transfer machines apply dye onto stretched socks placed over specialized aluminum mandrels, eliminating seam gaps entirely.
3. Waterless Eco-Inks & Zero-Wastewater Production
Next-gen waterless disperse ink formulations eliminate post-transfer washing cycles. Combined with solar-powered heat pressing lines in our factory, environmental footprint per unit is reduced by 68% compared to traditional wet dyeing processes.
Our Corporate Infrastructure: Why Global Brands Partner With Us
Operating as an integrated OEM/ODM manufacturing hub, we bridge the gap between creative design concepts and bulk retail delivery. From custom sock knitting to full-package cut and sew activewear, our facility provides comprehensive end-to-end oversight.
1. Low MOQ & Agile Batch Production
We eliminate high inventory risk for boutique brands and growing startups. While conventional textile mills demand 2,000+ units per style, our modular floor planning allows minimum order quantities starting at just 50 to 100 pieces per style. This enables agile testing of seasonal drops and rapid re-order scaling based on real-time sell-through metrics.
2. Precision Material Sourcing & GSM Verification
Our raw yarn inventory includes combed long-staple cotton, moisture-wicking CoolMax poly blends, Dupont Lycra, and silver-infused antimicrobial synthetic fibers. Every batch of fabric undergoes strict weight checks (GSM tolerance within ±3%) and pre-shrinkage washing trials prior to cutting.
3. Rigorous 8-Stage Quality Assurance (AQL 2.5 Standard)
Quality control is embedded directly into the sewing line. Every single garment or sock batch progresses through eight standardized checkpoints:
- Stage 1: Raw Fiber & Dye Lot Inspection - Spectrophotometer shade verification against Pantone TPX/TCX standards.
- Stage 2: Pattern Drafting & CAD Mockup Approval - Digital grading across XS to 5XL sizing specs.
- Stage 3: Pre-Production Sample Sign-Off - Fit and wear testing before bulk cutting approval.
- Stage 4: Automated Laser Cutting - Precision panel trimming with zero fraying.
- Stage 5: Sublimation Print Curing & Color Registration Check - DPI clarity and transfer alignment.
- Stage 6: In-Line Stitching & Seam Strength Tension Test - 4-needle 6-thread flatlock integrity.
- Stage 7: Post-Assembly Metal Detection & Needle Sweep - Consumer safety assurance.
- Stage 8: Final Packaging & Barcode Audit - Custom polybagging, hangtag placement, and export box tagging.
B2B Buyer FAQ: Sublimation Sourcing & Custom Manufacturing
Ready to Elevate Your Apparel Line?
Partner with China’s premier sublimation printing and apparel manufacturing export facility. Get custom quotes, fabric samples, and technical CAD mockups in under 24 hours.
Inquire Now