Featured Bulk Apparel & Custom Hosiery Collections
Low MOQ custom cut-and-sew solutions, technical activewear, and custom apparel manufactured to strict AQL 2.5 quality standards.
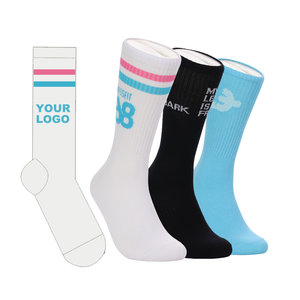
Custom Socks Factory No Minimum High Quality Cotton White Socks
- 100% Combed Cotton & Elastic Spandex
- Custom Jacquard & Embroidered Logo
- Low MOQ / Agile Sample Rounds
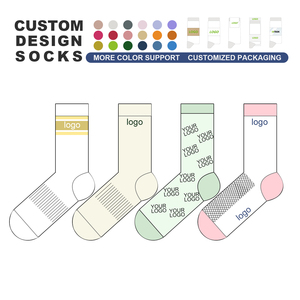
Custom Design Cotton Socken Personalized Embroidered Men Tube Socks
- High-Density Embroidery Crafting
- Reinforced Heel & Seamless Toe
- Bulk Wholesale & Stock Lot Pricing
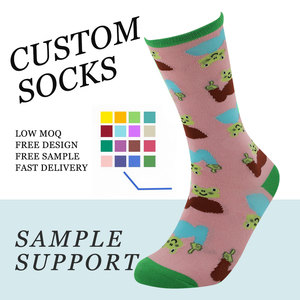
Unisex Crew Personalized Jacquard Logo Customized Athletic Socks
- Breathable Moisture-Wicking Knit
- Custom Color Matching (Pantone TCX)
- Low MOQ for E-Commerce Startups
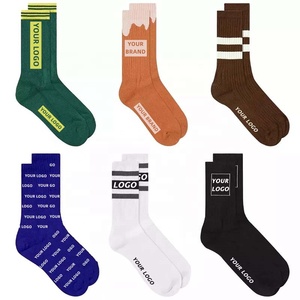
Designer Jacquard Knitted 100% Cotton Thick Anti-Bacterial Socks
- Silver-Ion Anti-Bacterial Treatment
- Heavyweight Terry Cushioning
- Private Label Brand Customization
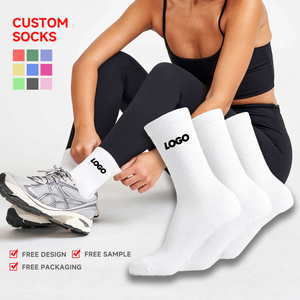
Personalized White Letter Custom Gym Crew Socks for Women
- Precision Lettering & Graphic Weaving
- Soft Compression Arch Support
- Custom Retail Packaging Bags Included
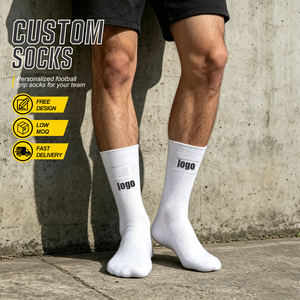
Breathable Performance Sports Basketball Crew Socks for Men
- High-Impact Zone Cushioning
- Nylon & Spandex Durable Blend
- Sublimated or Knitted Logo Options
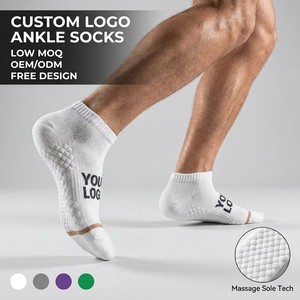
Custom Logo Massage Ankle Socks Anti-Blister Breathable Low-Cut
- Ergonomic Sole Massage Dots
- Anti-Slip Heel Grip Technology
- Luxury Gift & Amenity Packaging
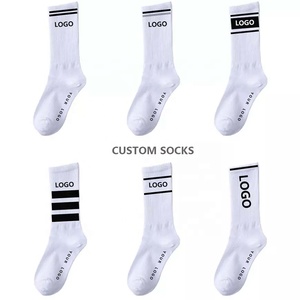
OEM Fast Sample Custom Logo Running Athletic Basketball Socks
- 7-Day Rapid Prototyping Lead Time
- Graded Size Specifications (S-XL)
- Factory Direct Bulk Pricing Tiers
Executive Sourcing Report: Navigating China Bulk Clothing Manufacturing in 2026
The global textile and apparel procurement landscape is experiencing a profound paradigm shift. Modern apparel brands, e-commerce retailers, and wholesale distributors are moving away from traditional mass-volume inventory risks toward agile, data-driven sourcing models. Partnering with top-tier China bulk clothing manufacturers and suppliers now requires more than just searching for low unit costs; it demands deep operational integration, fabric traceability, rapid prototyping capabilities, and strict adherence to international quality standards.
As a established OEM/ODM manufacturing force with strategic hubs and production facilities in China alongside domestic consultation teams in North America (Charlotte, NC & Los Angeles, CA), our integrated manufacturing infrastructure bridges the gap between Asian industrial supply chain density and Western retail requirements. Whether launching an emerging private label brand or scaling an established streetwear line, understanding the technical nuances of garment manufacturing is essential for preserving gross margins and securing brand equity.
Core Enterprise Capabilities & Infrastructure
Why leading global apparel brands rely on our full-package cut-and-sew apparel production floor.
Full-Package Cut & Sew
From initial hand sketches and CAD tech packs to graded master pattern making, marker planning, precision fabric cutting, and assembly line sewing. We manage every step under one roof to eliminate vendor fragmentation.
Rigorous Fabric Sourcing & Testing
Direct mill relationships enable access to GOTS-certified organic cotton, recycled polyester (rPET), heavyweight French terry, performance spandex blends, and technical moisture-wicking knits. Every batch undergoes GSM density and shrinkage verification.
End-to-End Private Labeling
Custom woven neck tags, printed care labels, customized hangtags, recycled poly bagging, barcoding, and retail-ready shipper boxes. Garments leave our facility prepped directly for 3PL warehouse fulfillment.
Strategic Procurement Trends: The Next Decade in Apparel Manufacturing
Sourcing apparel in bulk requires anticipating macroeconomic trends, technological breakthroughs, and shifting consumer expectations. Buyers who adapt early to these four macro-trends will capture significant market share.
Agile Low-MOQ Production Scaling
The era of forcing brand owners to order 1,000+ units per colorway is over. Modern Chinese manufacturing hubs utilize modular sewing lines that accommodate 50 to 100 piece minimums per style. This agility enables brands to test micro-collections, gather real-time consumer conversion data, and reorder winning SKUs within 25 business days, eliminating excess deadstock.
Traceable & Sustainable Textile Chains
Global regulations (such as ESG disclosure laws and EU digital product passports) require full transparency across raw material sourcing. Leading bulk suppliers now provide mill-level certification for GOTS organic cotton, OEKO-TEX Standard 100 non-toxic dyes, and Global Recycled Standard (GRS) synthetic fibers, ensuring compliance and consumer trust.
3D CAD Design & Digital Prototyping
Before cutting physical fabric, 3D digital garment sampling allows design teams to evaluate drape, stress tension, seam placement, and print scaling on digital avatars. This reduces physical sample iterations from 4 rounds down to 1, cutting pre-production timelines by up to 60% and saving substantial sampling costs.
Smart Functional Textiles & Performance Treatments
Consumer demand is rapidly pivoting toward multifunctional garments. Bulk production now routinely incorporates embedded technology: silver-ion anti-microbial coatings, UPF 50+ UV blocking, temperature-regulating phase-change materials, and eco-friendly durable water repellent (DWR) finishes for activewear and casual apparel alike.
Advanced Decoration & Customization Tech
Unlocking elevated brand positioning through state-of-the-art fabric embellishment techniques.
High-Density Screen Printing
Plastisol, water-based, and discharge printing alongside tactile puff inks. Every print run is heat-cured and subjected to 50+ industrial wash cycles to guarantee zero cracking or color degradation.
Precision 3D Puff Embroidery
Digitized embroidery files mapped to Tajima multi-head industrial machines. From flat tonal stitching to high-rise 3D foam puff embroidery on fleece hoodies, caps, and heavy cotton socks.
Deep-Dye Sublimation
All-over digital sublimation printing for polyester performance wear and activewear. Colors bond directly to fabric fibers at a molecular level, preventing fading, peeling, or loss of breathability.
8-Stage Bulk Manufacturing Lifecycle
How your bulk apparel order moves seamlessly from technical concept to global container delivery.
Consultation & Quote
Reviewing tech packs, target market specs, fabric GSM, color codes, and desired order quantities to deliver a transparent, binding quote.
CAD & Pattern Making
Transforming sketches into scaled CAD patterns with precise measurement points across all graded size ratios (XS through 3XL).
Fabric Sourcing
Lab-dyes (Pantone TCX matching) and custom yarn knitting. Lab dips and fabric hand-feel swatches sent for client sign-off.
Pre-Pro Sample
Creating a physical fit sample. Physical sample sent for real-world wear testing, fit adjustment, and construction verification.
Bulk Cut & Sew
Computerized laser cutting tables ensure precision panel alignment, followed by line stitching on specialized sewing stations.
Print & Embellish
Applying screen prints, custom embroidery, transfer patches, or custom jacquard weaves under controlled environmental standards.
AQL 2.5 Inspection
Comprehensive quality control: seam strength stress tests, thread trimming, dimensional measurement audits, and wash colorfastness checks.
Pack & Export
Individual poly-bagging, inner carton packing, custom labeling, and tracked air/sea freight shipping with full customs clearing paperwork.
Frequently Asked Procurement Questions
Everything enterprise apparel buyers, brand founders, and sourcing directors need to know about manufacturing in China.
What is the minimum order quantity (MOQ) for custom bulk apparel?
How long does sampling and bulk manufacturing take?
What information is required to receive an accurate factory quotation?
- Garment Tech Pack or physical reference sample.
- Fabric composition and target GSM weight (e.g., 100% Combed Cotton, 320 GSM).
- Order quantity breakdown per style and size ratio distribution.
- Specific decoration methods, artwork size, and placement coordinates.
- Custom branding details (woven tags, printed care labels, custom packaging bags).
How do you ensure quality control across bulk production runs?
Can you handle private labeling, custom tags, and custom retail packaging?
What shipping options and export documentation do you handle?
Ready to Scale Your Bulk Clothing Manufacturing?
Partner with China's premier bulk apparel manufacturer. Send us your tech pack, sketch, or physical sample to receive custom fabric swatches, technical design feedback, and a competitive factory-direct quotation within 24 hours.