Featured OEM & ODM Custom Pillowcase Series
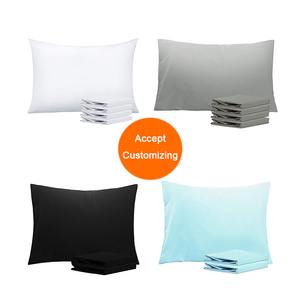
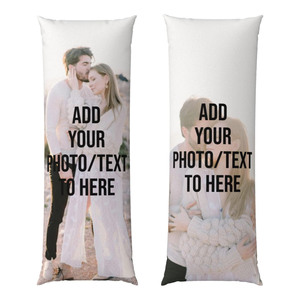
Explore our export-grade pillowcase series tailored for retail apparel brands, luxury hospitality chains, e-commerce private labels, and promotional distributors. Engineered for high wash-durability and custom branding.
Strategic Sourcing & Manufacturing Guide for China Pillowcase Export
Navigating the global textile ecosystem requires more than simply finding a sewing facility; it demands a deep technical understanding of fabric substrate engineering, yarn count mechanics, high-precision dye chemistry, and export logistics compliance. As a leading specialized manufacturer and exporter based in China's premier textile industrial hubs, our manufacturing infrastructure bridges the gap between boutique custom brands and high-volume commercial importers. Whether supplying luxurious 100% Mulberry silk cases for hair-care beauty brands, high-density 280G Dutch velvet throw covers for home decor retailers, or GOTS-certified organic bamboo pillowcases for eco-conscious hotel groups, China's integrated supply chain delivers unassailable cost efficiency, technical precision, and rapid production turnaround.
In accordance with global standards such as OEKO-TEX Standard 100, ISO 9001 quality management, and strict AATCC laundering performance metrics, modern OEM/ODM custom pillowcase production has evolved beyond basic stitching. Procurement executives must evaluate suppliers based on Information Gain—focusing on raw yarn sourcing origin, fiber staple length, digital reactive printing color spectrum precision, automated edge-overlocking seam strength, and retail-ready private labeling packaging integrations.
Enterprise Manufacturing Advantages & Core Capabilities
Our floor planning and vertical integration eliminate the classic friction points associated with overseas textile procurement. By maintaining complete control over fabric sourcing, pattern grading, cut-and-sew operations, decoration lines, and final cartoning, we guarantee transparent timelines and zero compromise on product consistency.
Precision Fabric Sourcing & GSM Control
We source raw greige fabrics directly from audited yarn mills. Every batch undergoes strict Grams per Square Meter (GSM) verification, fiber staple audit, and pre-wash shrinkage calibration to prevent sizing shifts post-laundering.
Advanced Printing & Decoration Lines
Utilizing high-speed Italian digital reactive printing machinery, Japanese AJS sublimation setups, and multi-head Tajima embroidery stations, we achieve photo-realistic image transfer, vibrant CMYK+OG color gamut matching, and 4.5+ wash colorfastness.
Agile Small-Batch & Bulk Floor Planning
Unlike rigid industrial facilities requiring thousands of pieces per colorway, our flexible cut-and-sew lines accommodate low initial orders (50 to 100 pieces per style), allowing brands to test market demand prior to scaling into bulk production drops.
8-Step Rigorous Quality Control (QC) Protocol
Every pillowcase unit moving through our assembly lines passes an exhaustive 8-step quality framework:
- Fabric Inspection: Automated optical scanning for yarn slubs and weaving flaws.
- Dye Lot Consistency: Spectrophotometer testing against Pantone TCX/TPG standards.
- Precision Cutting: Laser-guided pattern slicing ensuring exact dimensional tolerances (±0.5 cm).
- Seam Stress Testing: Dual-needle safety stitch and 5-thread overlocking tension validation.
- Hardware Verification: Concealed zipper pull testing up to 500 open/close cycles (YKK standard).
- Laundering & Shrinkage Test: Sample wash cycles at 40°C to verify dimensional retention.
- Ironing & Finishing: Industrial steam pressing for clean fold aesthetic.
- Final Carton Audit: Barcode scanning, moisture absorber insertion, and drop-test packaging certification.
Full-Package Private Label & Fulfilment Integration
We transform plain manufactured soft goods into retail-ready consumer products. Our in-house packaging department executes complete private label workflows:
- Custom Labeling: High-density satin woven neck tags, printed care labels, and organic cotton ribbon tags.
- Boutique Hangtags: Soft-touch foil stamped paperboard hangtags with barcode stickers.
- Eco-Friendly Polybags: Frosted TPU zipper bags, biodegradable PLA bags, or printed rigid gift boxes.
- Barcoding & Master Shipping: Amazon FBA label compliance, palletization, and DDP air/sea tracking documentation directly to global distribution centers.
Technical Material Analysis & Specifications Comparison
Selecting the ideal textile substrate is critical to aligning product performance with your Target Buyer Persona. The matrix below outlines technical specifications for our five primary export pillowcase fabric categories:
| Fabric Category | Weight / Density (GSM / Momme) | Key Technical Properties | Ideal Target Market Application | Recommended Printing Method |
|---|---|---|---|---|
| 100% Pure Mulberry Silk | 19, 22, or 25 Momme (6A Grade) | Hypoallergenic, ultra-low friction, amino acid enriched, zero hair moisture depletion | Luxury Skincare Brands, Premium Beauty Retailers, Boutique Spas | Reactive Digital Printing / Monogram Embroidery |
| Organic Bamboo Viscose | 300 TC - 400 TC / 140 GSM | Thermoregulating, moisture-wicking, silky drape, sustainable bio-degradable fibers | Eco-Friendly Bedding Brands, Hotel Chains, Wellness Boutiques | Eco-Friendly Water-Based Pigment Print / Screen Print |
| Combed Long-Staple Cotton | 300 TC - 800 TC / 120-180 GSM | High tensile strength, breathable, crisp hand-feel, withstands commercial laundering | Hospitality Industry, Residential Bedding Brands, Institutional Procurement | Digital Reactive Print / Rotary Screen Print |
| 280G Heavyweight Dutch Velvet | 280 GSM Pile Weight | Plush texture, rich color depth, abrasion resistant, non-shedding synthetic pile | Home Decor Retailers, Interior Design Studios, Custom Throw Pillows | Heat Transfer Dye Sublimation / 3D Embossing |
| Ultra-Soft Microfiber Poly | 85 - 110 GSM Brushed Microfiber | Wrinkle-resistant, fast-drying, lightweight, high cost-efficiency for mass promos | E-Commerce Mass Retail, Promotional Giveaways, Merchandise Drops | High-Definition All-Over Sublimation Printing |
Future Industry Trends in Custom Pillowcase Manufacturing
The global textile and home bedding industry is undergoing a massive transformation driven by changing consumer values, technological breakthroughs in digital manufacturing, and stringent environmental regulations. Suppliers in China are leading this transition through significant R&D investments and factory automation.
Zero-Discharge Green Dyeing
Environmental sustainability is no longer optional. Modern China processing facilities employ closed-loop water filtration systems and OEKO-TEX certified non-toxic dyestuffs, drastically reducing chemical runoff and carbon intensity per linear meter of printed fabric.
Bio-Active & Smart Yarns
Next-generation pillowcases integrate functional performance features directly into yarn composition. Demand is surging for copper-infused anti-bacterial fabrics, phase-change cooling materials (PCM), and collagen-coated threads designed to protect skin hydration overnight.
On-Demand On-Shore Sourcing
E-commerce brands are shifting away from massive annual inventory holdings toward agile, small-batch replenishment. High-speed digital reactive printers enable direct file-to-fabric output without screen setup costs, supporting micro-drop catalog strategies.
Information Gain Insight: The Closure Engineering Shift
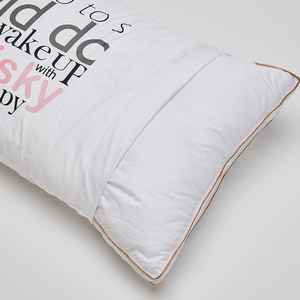
While traditional envelope closures (with a standard 15cm overlap) remain popular in European markets due to simplicity, global e-commerce brands are increasingly specifying invisible YKK zippers concealed beneath a 3mm fabric piping lip. This technical design shift prevents pillow inserts from slipping during sleep, creates a seamless aesthetic for 3D digital prints, and elevates perceived retail value by an estimated 25-30%.
Strategic B2B Sourcing & Logistics Optimization
Maximizing gross profit margins on imported pillowcases requires a clear procurement framework. Overseas brand managers must account for duty tariffs, freight volume density, sample approval protocols, and land-cost calculations.
Reducing Freight Costs via Vacuum Compression
Textiles are inherently bulky items. Shipping hollow pillow covers uncompressed severely inflates volumetric sea freight calculations (CBM). Our factory utilizes industrial vacuum sealing equipment to compress packaged pillowcases into compact master cartons, reducing shipping volume by up to 65%. This optimization lowers per-unit ocean and air freight costs substantially, directly boosting your net landed margin.
Navigating OEM vs. ODM Sourcing Workflows
We accommodate both Original Equipment Manufacturing (OEM) and Original Design Manufacturing (ODM) models:
- OEM Workflow: You supply complete tech packs, Pantone color references, artwork vector files (.AI / .EPS), and fabric GSM specs. We build exact prototype samples for physical sign-off.
- ODM Workflow: Select from our extensive library of pre-tested pattern templates, trendy print designs, and standard material compositions, applying your logo and branding for rapid market deployment.
Frequently Asked B2B Procurement Questions
Direct answers to common questions asked by brand owners, sourcing directors, and procurement managers prior to initiating production.
Ready to Scale Your Pillowcase Line with China's Premier Manufacturer?
Connect directly with our senior textile engineering team. Send your tech pack, design files, or sourcing inquiry today for an instant factory quote and sample swatch kit.
Inquire Now