Featured Wholesale Blank Apparel & Custom Accessories
Explore our factory-direct blank inventory engineered for private label custom embroidery, screen printing, and brand scaling.
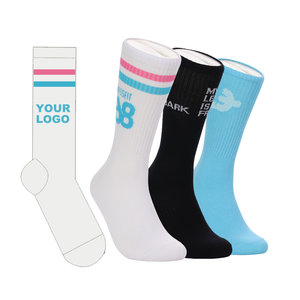
Custom Socks Factory Custom No Minimum Order High Quality Cotton White Socks Custom Socks With Logo
Premium combed cotton athletic crew blanks featuring reinforced toe-heel cushioning and 168-needle high density weave.
Send an Inquiry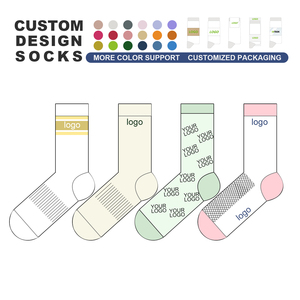
Custom Design Cotton Socken Personalized Logo Embroidered Men Tube Fashion Socks Sox Crew Dress Socks Stock Lot
Luxury ribbed knit blanks tailored for precise logo embroidery, elastane arch support, and anti-slip stretch durability.
Send an Inquiry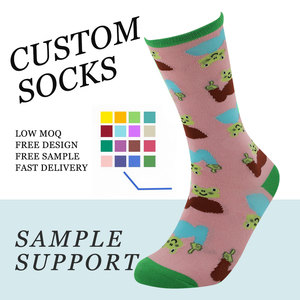
Unisex Crew Personalized Design Your Own Logo Sock Customized Socks Jacquard Custom Logo Socks Low MOQ
Seamless tube sock blanks optimized for multi-color jacquard pattern integration with breathable organic cotton blend yarns.
Send an Inquiry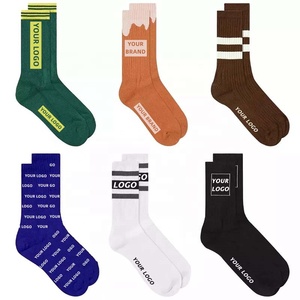
Designer Jacquard Knitted Crew 100% Cotton Thick Anti-Bacterial Brands Socks Casual Letter Bottom Logo Funny Sports Custom
Heavyweight plush terry bottom blanks infused with anti-bacterial silver ion technology for street fashion brands.
Send an Inquiry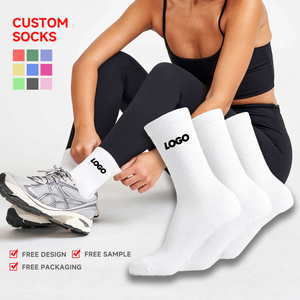
Personalized White Letter Socks Custom Logo Gym Crew Socks for Women Embroidery Sport Athletic Cotton Socks
Ergonomic fit performance blanks engineered with moisture-wicking technology and double-layered elastic rib cuffs.
Send an Inquiry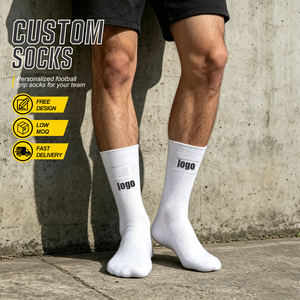
Breathable Sports Basketball Crew Men Socks Custom Socks Logo Sport Socks Running
High-impact absorption sole padding with mesh breathability zones. Ideal for custom streetwear and activewear lines.
Send an Inquiry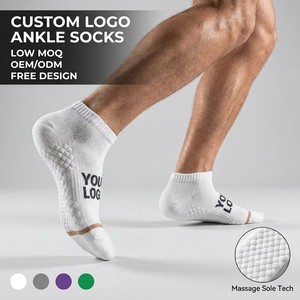
Custom Logo Massage Ankle Socks Anti-Blister Cotton Breathable Low-Cut Luxury Gift Hotel Amenity
Low-profile invisible ankle socks featuring silicone heel grips and massage-texture sole knits for hotel & retail custom packs.
Send an Inquiry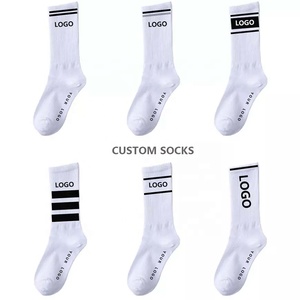
OEM Moq Fast Sample Oem Custom Logo Crew Socks Men Running Sport Socks, Cycle Athletic Custom Logo Basketball Socks
Rapid-turnaround OEM custom crew blanks with 7-day prototyping and 25-day bulk execution for international athletic brands.
Send an InquiryEmpirical Manufacturing Operations & Benchmark Data
Data-driven performance metrics reflecting our supply chain efficiency, quality pass rates, and international export capabilities.
1. Strategic B2B Blueprint: Navigating China’s Blank Clothing Ecosystem
The global apparel commerce landscape has undergone a seismic shift toward print-on-demand flexibility, rapid restocking models, and premium blank garment foundation strategy. As modern clothing labels, independent boutique brands, and corporate merchandisers strive to establish distinct market positions, the baseline garment quality—commonly referred to as the "Blank”—has emerged as the single most decisive factor governing customer retention, brand equity, and profit margins. Sourcing blank apparel directly from specialized Chinese manufacturing hubs offers an unmatched combination of fabric innovation, cost efficiency, scalable customization, and structural durability.
Historically, blank apparel procurement was constrained by rigid wholesale minimums, uninspired boxy cuts, inconsistent fabric grammage (GSM), and unpredictable dye-lot variations. Modern tier-1 Chinese blank clothing suppliers and exporters have completely re-engineered this paradigm. By integrating advanced vertical knitting mills, automated laser-cutting tables, eco-friendly dye houses, and dedicated short-run assembly lines, leading Chinese manufacturers provide fashion brands worldwide with retail-ready blank foundations. Whether you require heavyweight 450 GSM fleece hoodies, combed ring-spun 240 GSM cotton t-shirts, high-density gauge knit socks, or technical activewear blanks, understanding the nuances of China's blank apparel ecosystem is essential for optimizing your global supply chain.
Standard commodity blanks often suffer from post-wash shrinkage exceeding 8-12%, seam twisting, and surface pilling. Leading Chinese exporters utilize pre-shrunk combed cotton, reactive dyeing techniques, and silicone soft washes to achieve dimensional stability under 3% post-wash variance, giving private labels a significant competitive advantage in customer satisfaction.
2. Enterprise Core Strengths & Vertical Manufacturing Advantages
Bridging the gap between raw fabric sourcing, precision pattern design, and retail-ready finished apparel delivery.
Vertical Fabric Sourcing & GSM Controls
We maintain direct integration with certified yarn spinners and dye mills. Every fabric roll undergoes rigorous weight verification (GSM checks), fiber composition lab tests, and color-fastness grading to ensure absolute consistency across bulk dye lots.
Low MOQ Short-Run Floor Planning
Unlike legacy factories requiring 1,000+ units per style, our operational lines are optimized for agile production runs starting at just 50 to 100 pieces per style, allowing growing labels to test new colorways and fits without inventory tie-up.
Full-Package Private Label Customization
From custom woven neck tags, printed satin care labels, and branded drawstrings to eco-friendly custom polybags and barcoded shipping cartons—our end-to-end service delivers fully branded garments ready for immediate retail fulfillment.
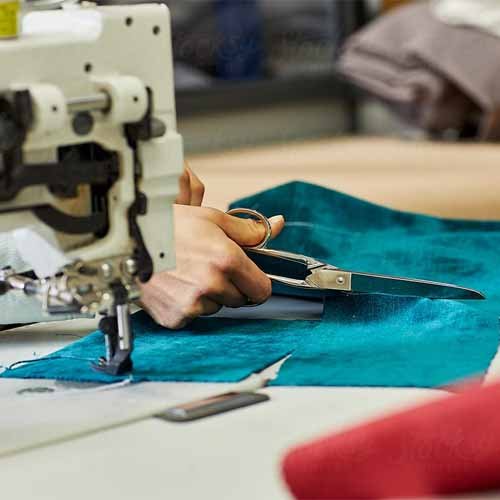
Precision Pattern Grading & Automated Cutting
CAD-assisted marker planning ensures zero material waste and identical sizing specs from XS to 3XL across every single cutting cycle.
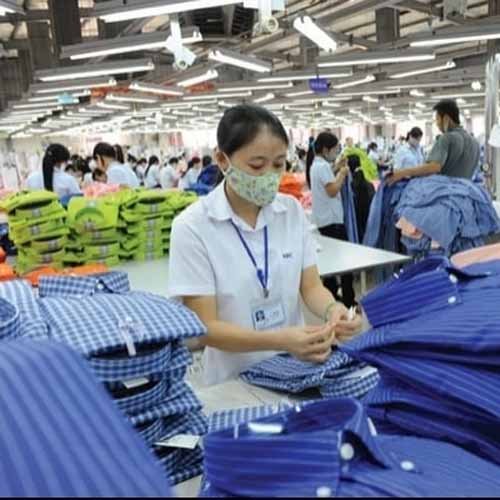
Rigorous Multi-Stage Quality Inspection
Inline seam stress testing, needle-detector scanning, wash-fastness validation, and dimensional tolerance checks guarantee flawless finished goods.
3. Blank Apparel Technical Specifications & Craftsmanship
To assist apparel buyers and brand directors in making informed sourcing decisions, the table below outlines our standardized technical parameters across major blank product categories manufactured in our facilities:
| Apparel Category | Standard Blank GSM Range | Primary Fiber Compositions | Recommended Decoration Methods | Sampling Lead Time |
|---|---|---|---|---|
| Heavyweight T-Shirts | 220 GSM - 300 GSM | 100% Combed Ring-Spun Cotton / Organic Cotton | Screen Printing, DTG, Puff Ink, Embroidery | 7 - 10 Days |
| Streetwear Hoodies & Sweats | 380 GSM - 500 GSM | French Terry / Fleece (100% Cotton or CVC Blends) | High-Density Embroidery, Chenille Patch, Screen Print | 8 - 12 Days |
| Athletic & Casual Socks | 168N - 200N Gauge | 80% Combed Cotton / 17% Polyester / 3% Spandex | Jacquard Weave, Custom Embroidery, Grip Printing | 5 - 7 Days |
| Seamless Leggings & Activewear | 240 GSM - 320 GSM | Nylon 66 / Spandex Blends / Recycled Polyester | Sublimation Printing, Heat Transfer Silicone Logo | 10 - 12 Days |
| Denim Apparel & Outerwear | 12 oz - 16 oz Denim | 100% Cotton Denim / Ring-Spun Twill | Enzyme Wash, Laser Distressing, Leather Patch | 12 - 15 Days |
Every garment produced on our facility lines is calibrated to withstand repeated industrial laundries without losing structural memory, collar elasticity, or softness. We provide custom lab-dip color matching against Pantone TCX/TPG color codes within 5 business days.
4. Eight-Stage Standardized OEM/ODM Production Workflow
From initial CAD concept to packed shipping cartons, our transparent workflow eliminates operational bottlenecks.
Comprehensive review of artwork, fabric specs, sizing ratio, and custom decoration details.
Digital pattern drafting and marker optimization to ensure ergonomic garment fit.
Mill procurement of pre-shrunk yarn, custom Pantone dyeing, and lab-dip sign-off.
Physical sample construction for tactile wear-testing and fit approval before bulk cutting.
Automated laser and knife cutting of graded pattern panels with minimal tolerance.
Embroidery, screen printing, or sublimation followed by high-tensile seam stitching.
100% thread trimming, dimensional measurement check, iron pressing, and spot cleaning.
Individual polybagging, custom inner boxes, tracked freight booking, and customs clearance.
5. Strategic Sourcing Forecast: Future Trends in Blank Apparel (2025–2030)
As global apparel buyers rethink their procurement blueprints, several key technological, environmental, and structural trends are defining the future of blank garment manufacturing and export from China:
1. Heavyweight Aesthetics & Vintage Washes
Streetwear brands are increasingly demanding ultra-heavyweight blanks (400 GSM+ tees, 500 GSM+ fleece) with specialized wash treatments such as acid washes, enzyme stonewashes, and pigment dips. Modern Chinese blank suppliers are upgrading wash house machinery to deliver consistent vintage aesthetic effects without compromising fabric structural integrity.
2. Eco-Friendly Yarns & GOTS Traceability
Environmental compliance is no longer optional. Sourcing directors are prioritizing GOTS-certified organic cotton, recycled polyester (rPET) derived from post-consumer plastic, and waterless dyeing processes. Chinese blank apparel exporters are embedding digital QR-code supply chain tracking, enabling brands to display verifiable sustainability metrics to end consumers.
3. Digital Micro-Manufacturing & Modular Blanks
To minimize stock risk, e-commerce retailers are transitioning toward modular blank stock—pre-manufactured neutral silhouettes kept in warehouse staging facilities, ready to be decorated via local DTG print fulfillment centers within 48 hours of consumer orders.
4. Functional Fiber Enhancements
Blanks are moving far beyond plain cotton. Thermoregulating yarns, anti-microbial bamboo charcoal knits, UV-blocking active coatings, and four-way stretch elastane blends are becoming standard expectations across lifestyle, sport, and workwear categories.
6. Macro Industrial Trends: China’s Upgraded Export Ecosystem
The global textile export landscape has entered a phase of high-tech transformation. While basic low-margin sewing has shifted toward emerging markets, China has solidified its position as the world's premier hub for complex technical knits, high-speed supply chain integration, and automated precision manufacturing. The synergy of regional industrial clusters—such as Guangdong for knitted streetwear and activewear, Zhejiang for premium socks and seamless garments, and Jiangsu for technical synthetic weaves—allows Chinese suppliers to achieve unparalleled manufacturing economies of scale.
Furthermore, digital transformation has dramatically reduced production cycle friction. Advanced CAD nesting algorithms, automated 3D virtual fitting simulations (such as Clo3D), and computerized automated sewing machinery allow custom blank garment orders to transition from design concept to physical export shipment faster than ever before. Foreign buyers benefit from shortened lead times, lower sample iteration costs, and strict compliance with international labor and environmental standards.
7. Frequently Asked B2B Procurement Questions (FAQ)
Clear, authoritative answers to common inquiries from apparel buyers, sourcing managers, and brand founders.
Ready to Scale Your Apparel Line With China’s Top Blank Supplier?
Partner with an established OEM/ODM exporter committed to premium fabric quality, flexible minimum orders, and guaranteed production timelines. Send your design sketch, tech pack, or product inquiry today.