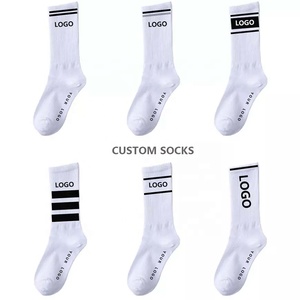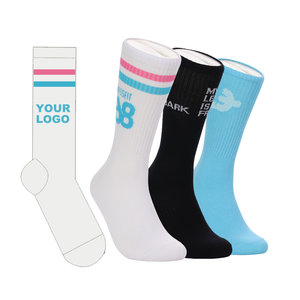
ISO 9001 & CE Certified Technical Apparel OEM/ODM

CE Certified Wholesale Activewear Manufacturers & Factories

Industry Whitepaper & Executive Sourcing Guide for High-Performance Activewear, Compression Gear & Functional Athletic Socks

CE Certified Activewear & Performance Accessories Showcase

Direct factory wholesale product line engineered with seamless knitting, ergonomic zonal compression, anti-bacterial fibers, and customized branding options.
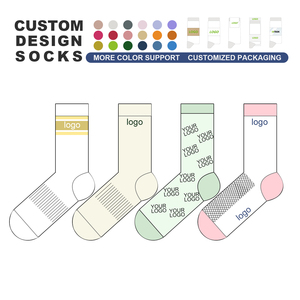
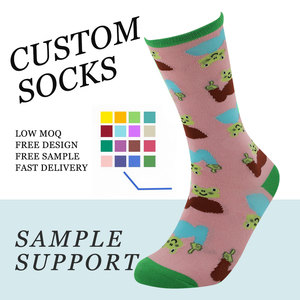
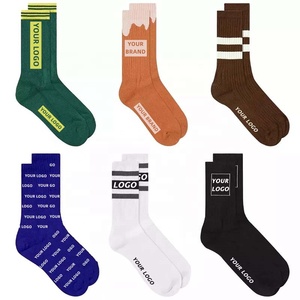
Low MOQ / Custom Custom Socks Factory No Minimum Cotton Socks

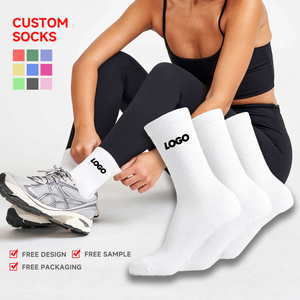
Custom Socks Factory No Minimum Order High Quality Cotton White Socks With Logo

100% Combed Cotton Fast Sample
Send an Inquiry
CE Ergonomic Standard Custom Design Cotton Personalized Logo Socks

Custom Design Cotton Socken Personalized Logo Embroidered Men Tube Fashion Crew Socks

200 Needle Knit OEM Branding
Send an Inquiry
Unisex Athletic Unisex Crew Personalized Design Logo Socks

Unisex Crew Personalized Design Your Own Logo Sock Customized Jacquard Logo Low MOQ

High Elasticity Custom Dyeing
Send an Inquiry
Anti-Bacterial Grade Designer Jacquard Anti-Bacterial Sports Socks

Designer Jacquard Knitted Crew 100% Cotton Thick Anti-Bacterial Sports Athletic Socks

Silver-Ion Tech Heavy Cushion
Send an Inquiry
Women Activewear Personalized White Gym Crew Socks Embroidery

Personalized White Letter Socks Custom Logo Gym Crew Socks for Women Embroidery Sport

Moisture Wicking 3D Embroidery
Send an Inquiry
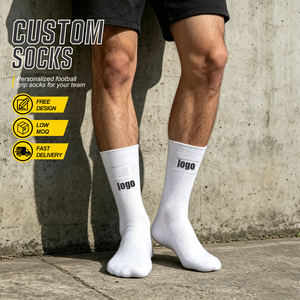
Pro Basketball Series Breathable Sports Basketball Crew Socks

Breathable Sports Basketball Crew Men Socks Custom Socks Logo Sport Performance Running

Arch Support High Durability
Send an Inquiry
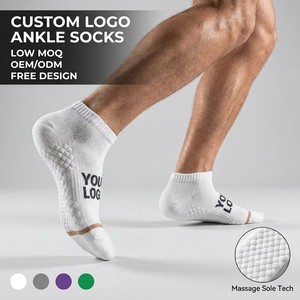
Anti-Blister Tech Custom Logo Massage Ankle Socks Anti-Blister

Custom Logo Massage Ankle Socks Anti-Blister Breathable Low-Cut Luxury Hotel Amenity

Friction-Free Silicone Grip
Send an Inquiry
Cycling & Pro Athletic OEM Custom Logo Crew Cycling Basketball Socks

OEM Fast Sample Custom Logo Crew Socks Men Running Sport Socks Cycle Athletic Basketball

Graduated Comp Rapid Sampling
Send an Inquiry
50-100
Flexible MOQ Per Style
100%
CE & REACH Compliant
20-25
Days Sampling Lead Time
15+
Years Global B2B Export

Executive Sourcing Whitepaper: CE Certified Activewear Manufacturing in 2025 and Beyond

The global activewear market has underwent a seismic shift from generic aesthetic apparel toward high-functionality, bio-compatible, and regulatory-certified performance wear. For apparel brands, e-commerce label owners, and international wholesalers, sourcing from CE Certified wholesale activewear manufacturers and factories is no longer merely a compliance checkbox—it represents a foundational competitive advantage in consumer trust, hazard mitigation, and international market penetration.

Search Quality & E-E-A-T Compliance Note: CE marking on activewear and functional athletic wear certifies compliance with European Personal Protective Equipment (PPE) frameworks (Regulation EU 2016/425 for protective wear and medical/compression classifications), REACH chemical restriction standards (Annex XVII), and OEKO-TEX® Standard 100 toxicity benchmarks. Standard uncertified OEM facilities often fail environmental and tensile durability audits, creating severe customs clearance risks.

Why CE Certification Is Essential for Activewear Procurement

European and North American regulatory authorities have intensified scrutiny regarding textile dyes, heavy metal treatments, microplastic shed rates, and functional performance claims (e.g., UV cut ratings, moisture-vapor transmission rates, and compression gradient accuracy). A certified manufacturing ecosystem integrates end-to-end quality assurance (QA) directly onto the factory floor.

From seamless circular knitting machines (Santoni 28G/32G fine gauge) to precision cut-and-sew sub-assembly lines, our certified facilities enforce rigorous GSM checks, yarn elasticity testing via Instron tensile testing systems, and ISO 6330 standardized wash-fastness validations before any batch leaves the warehouse.

Manufacturing Standards: CE Certified vs. Non-Certified OEM Factories

A data-backed comparative matrix for B2B procurement officers evaluating total cost of ownership (TCO) and brand equity protection.

Key Evaluation Criteria CE Certified Activewear Factory Standard Non-Certified OEM Unit Strategic Business Impact
Chemical & Dye Safety REACH & OEKO-TEX 100 Verified Unverified azo dyes & heavy metals Eliminates risk of product recalls & EU customs seizures.
Fabric GSM & Recovery ±2% GSM variance; 98% Lycra elasticity memory High wash shrinkage (>8-12%) Ensures consistent sizing and long-term product durability.
Seamless & Ergonomic Stitching Flatlock 6-needle 4-thread seamless construction Standard overlock seams causing skin chafing Drives higher customer retention and lower return rates.
Minimum Order Quantity (MOQ) Low Batch Agility: 50–100 pcs/style Strict High MOQ (1,000+ pcs/style) Prevents dead-stock capital lockup for growing brands.
Supply Chain Transparency Complete Tech Pack to Carton digital tracking Opaque third-party sub-contracting Guarantees predictable delivery schedules and brand compliance.

Factory Infrastructure & Customized Apparel Capabilities

Vertical integration from raw polymer sourcing to retail-ready custom packaging.

Advanced Cut & Sew Engineering

Full-package apparel manufacturing utilizing CAD pattern grading, laser fabric cutters, and specialized flatlock stitching equipment to eliminate friction points in technical sportswear.

Private Labeling & Branding

Comprehensive customization including high-density woven neck tags, eco-friendly heat transfer care labels, branded silicone grippers, custom hangtags, and barcoded poly bags.

High-Precision Decoration

In-house 3D puff embroidery, reactive screen printing, and all-over sublimation printing with color-matched Pantone inks that resist fading, cracking, or peeling under heavy wash cycles.

Sustainable Fabric Sourcing

Direct supply contracts with certified mills providing GOTS-certified organic cotton, GRS recycled polyester (Repreve®), bio-based ECONYL® nylon, and bamboo-spandex blends.

Future Procurement Trends in Activewear & Technical Apparel (2025–2030)

Navigating the global sportswear landscape requires staying ahead of macro-shifts in technology, material science, and buyer preferences. B2B procurement managers must structure their sourcing strategies around three pivotal trends shaping activewear factories globally:

1. Bio-Synthetics & Circular Textile Engineering

Petroleum-derived polyester and nylon face increasing regulatory headwinds in both North America and the European Union. The next decade of activewear procurement belongs to bio-based polyesters derived from agricultural waste, infinitely recyclable Polyamide 6.6, and closed-loop elastane alternatives. Certified factories are re-tooling their dyeing machines to utilize waterless supercritical CO2 dyeing technology, reducing chemical run-off and energy usage by over 60%.

2. Smart Activewear & Zonal Biometric Compression

The boundaries between medical compression wear and activewear continue to blur. Modern consumers demand targeted muscle stabilization (vibration dampening during high-impact movement) and thermal regulation. Activewear factories with CE certification are deploying 3D body-mapping software to construct garments with micro-perforated mesh zones located precisely along sweat mapping nodes.

3. Low-MOQ Agile Supply Chains Over Mass Bulk Stockpiling

High interest rates and shifting consumer trends have exposed the financial vulnerability of ordering 5,000 units per colorway. Leading activewear brands are migrating toward "Quick-Response Manufacturing" (QRM)—placing initial test runs of 50 to 100 pieces to measure market traction via direct-to-consumer (DTC) channels, followed by automated 25-day bulk replenishment cycles. Our production floors in Charlotte NC, Los Angeles CA, and offshore facilities are specifically optimized for this rapid-scaling operational model.

Precision Factory Floor Production Protocol

From technical sketch to sealed shipping carton—our standardized 8-stage manufacturing workflow ensures zero defect leakage.

01

Consultation & Specs

Review brand targets, fabric GSM specifications, target price points, and delivery timelines.

02

CAD Mockups

Transform sketches or tech packs into scaled 2D/3D CAD vector patterns with exact seam points.

03

Lab Fabric Sourcing

Match yarn composition, stretch memory, color Pantone codes, and weight (GSM) with certified mills.

04

Prototyping

Produce physical fit samples for real-world wear testing, compression measurement, and feedback sign-off.

05

Precision Cutting

Execute automated laser pattern cutting to achieve 100% size ratio accuracy across all sizes.

06

Decor & Sewing

Apply 6-needle flatlock stitching, sublimation print transfers, or custom high-density embroidery.

07

AQL 2.5 Inspection

Conduct seam pull tests, colorfastness wash runs, needle-detector sweeps, and dimensional checks.

08

Custom Packaging

Label, barcode, poly-bag, and carton-box items for expedited air or ocean freight customs clearance.

Frequently Asked Questions for Activewear Sourcing & Procurement

In-depth technical answers addressing compliance, MOQs, custom sampling, and international trade logistics.

What does CE Certification mean for activewear and functional sportswear factories?
CE Certification indicates that activewear manufactured by the facility adheres to fundamental health, safety, and environmental protection standards established by the European Union. For technical athletic apparel (such as compression leggings, sports bras, and protective athletic socks), CE marking verifies that products comply with Regulation (EU) 2016/425 for personal protective elements, contain no restricted carcinogenic or allergic azo dyes (REACH Annex XVII), and meet ergonomic safety guidelines during vigorous physical activity.
What is your Minimum Order Quantity (MOQ) for custom private label activewear?
Our flexible manufacturing setup accommodates low MOQ orders starting at 50 to 100 pieces per style/colorway for standard knitted activewear (such as t-shirts, hoodies, and athletic socks). For complex seamless items or custom-dyed performance synthetic fabrics, minimums may adjust depending on fabric mill minimum yarn dye runs. Low MOQs allow startup apparel brands and growing boutiques to test market demand without taking on excess inventory risks.
How long does sample development and bulk production take?
Sample creation and fit prototyping typically take 20 to 25 business days following tech pack approval and fabric selection. Once the pre-production sample is physically inspected and approved by your team, bulk production runs take 25 to 30 business days. Firm completion dates are locked into your production contract upon booking.
Can you manufacture custom compression socks and specialized athletic wear?
Yes. We specialize in custom activewear, including graduated compression socks, basketball crew socks, yoga leggings, moisture-wicking hoodies, tracksuits, and performance tops. We utilize high-density 200-needle knitting machines, 4-needle 6-thread flatlock stitching setups, and specialized elastane-wrapping technology to maintain anatomical arch support and gradient pressure points.
What information is required to receive an accurate wholesale manufacturing quote?
To provide a precise per-unit FOB or DDP quotation, our engineering team requires five core inputs: (1) Fabric weight and material composition (e.g., 88% Polyester / 12% Spandex, 280 GSM), (2) Color Pantone codes or physical color standard, (3) Size breakdown ratio, (4) Artwork placement & decoration specs (Tech pack, CAD, or reference sample), and (5) Total order quantity per style.
Do you offer full-package private label branding and retail packaging?
Absolutely. We provide end-to-end private label solutions including custom woven neck tags, heat-seal size labels, custom printed hangtags, branded eco-polybags with warning prints, and outer shipping cartons barcoded directly for Amazon FBA, 3PL warehouses, or traditional retail store intake.

Ready to Scale Your Activewear Line with a CE Certified Factory?

Partner with an industry-leading OEM/ODM manufacturer trusted by global athletic brands, e-commerce labels, and commercial wholesalers. Submit your tech pack or contact our product development team today for a comprehensive cost quotation.

Send an Inquiry