Featured CE-Certified Custom Wear & Sock Lineups
Explore our industrial-grade, precision-knitted sock and custom apparel series. Each item features low minimum order quantities (MOQ), OEM logo customization, high-grade combed cotton yarn, and certified anti-bacterial ergonomic engineering.
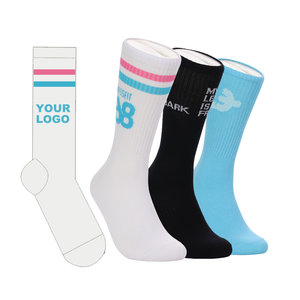
Custom Socks Factory Custom No Minimum Order High Quality Cotton White Socks Custom Socks With logo
- Material: 80% Combed Cotton / 17% Nylon / 3% Spandex
- Tech: 200-N needle count high-density weave
- Compliance: OEKO-TEX Standard 100 & CE
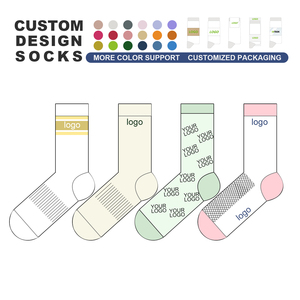
Custom Design Cotton Socken Personalized Logo Embroidered Men Tube Fashion Socks Sox Crew Dress Socks Stock Lot
- Craft: Precision 3D logo embroidery
- Cushioning: Reinforced heel and seamless toe
- Application: Men's Business & Casual Fashion
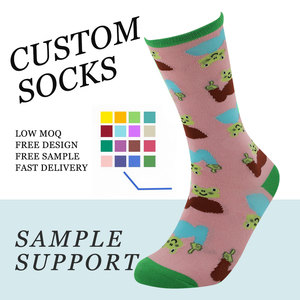
Unisex Crew Personalized Design Your Own Logo Sock Customized Socks Jacquard Custom Logo Socks Low MOQ
- Weave: Custom jacquard knit artwork placement
- Fit: Unisex elastic rib band control
- Minimums: Low MOQ options from 100 pairs/style
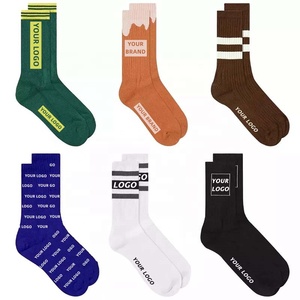
Designer Jacquard Knitted Crew 100% Cotton Thick Anti-Bacterial Brands Socks Casual Letter Bottom Logo Funny Sports Custom
- Technology: Silver-ion anti-microbial treatment
- Bottom Logo: Non-slip printed or knitted text
- Comfort: Extra thick terry sole impact absorption
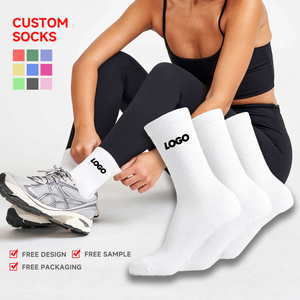
Personalized White Letter Socks Custom Logo Gym Crew Socks for Women Embroidery Sport Athletic Cotton Socks
- Feature: Moisture-wicking dynamic mesh top
- Branding: High-definition letter embroidery
- Durability: Pre-shrunk micro-fiber construction
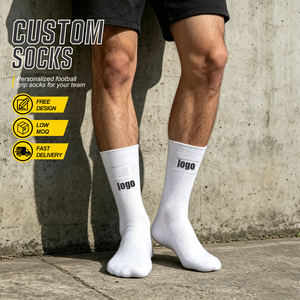
Breathable Sports Basketball Crew Men Socks Custom Socks Logo Sport Socks Running
- Structure: Ankle compression & arch support band
- Breathability: Zoned ventilation grid channels
- Standard: High-impact shock absorption design
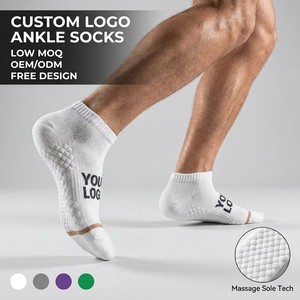
Custom Logo Massage Ankle Socks Anti-Blister Cotton Breathable Low-Cut Luxury Gift Hotel Amenity
- Speciality: Anti-friction heel tab & massage sole
- Market: Hospitality amenity & luxury retail gifting
- Packaging: Branded custom polybag or gift box
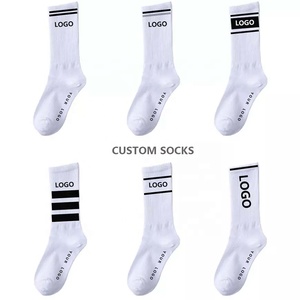
OEM Moq Fast Sample Oem Custom Logo Crew Socks Men Running Sport Socks, Cycle Athletic Custom Logo Basketball Socks
- Speed: 7-day rapid CAD prototyping & sampling
- Performance: High-stretch moisture-management yarn
- Customization: Full package OEM private label
CE Certification & Compliance Protocols in Global Custom Wear Exports
Navigating European Union directives and international quality standards for apparel importers, private labels, and commercial distributors.
In the contemporary global apparel trade, CE Certification (Conformité Européenne) is far more than a regulatory checkbox—it represents a comprehensive quality control framework that guarantees consumer safety, material non-toxicity, and structural durability. For fashion startups, corporate distributors, and sports apparel brands sourcing from overseas custom wear factories, ensuring strict alignment with CE standards and EU Personal Protective Equipment (PPE) Regulation (EU) 2016/425 is essential to prevent costly customs seizures and product recalls.
As a premier OEM/ODM custom apparel manufacturer operating export hubs across North America and Asia, our manufacturing workflows integrate CE compliance testing from yarn procurement to final carton sealing. Our enterprise facilities adhere strictly to ISO 9001 quality management systems and ISO 14001 environmental protocols, offering complete transparency across every link of the production chain.
| Regulatory Standard | Technical Scope & Testing Parameter | Factory Enforcement Protocol | B2B Buyer Business Benefit |
|---|---|---|---|
| CE PPE (EU 2016/425) | Ergonomic safety, tear resistance, and physical impact absorption. | Tensile strength testing on seam stitches; friction resistance checks. | Zero customs clearance friction in European ports. |
| REACH Annex XVII | Strict restriction of hazardous chemicals, heavy metals, and Azo dyes. | Spectrophotometer chemical screening; zero toxic chemical dying baths. | 100% skin-safe, hypoallergenic wear guarantee for consumers. |
| OEKO-TEX Standard 100 | Class I & II certification for direct-to-skin textile safety. | Certified organic cotton yarn sourcing & eco-friendly pigments. | Higher retail price point and premium brand positioning. |
| AQL 2.5 Quality Assurance | Defect tolerance threshold for mass bulk production exports. | Double-pass manual seam, print cure, and dimensional stability checks. | Under 0.1% defect rate upon warehouse delivery. |
Why Global Fashion Brands Partner With Our Factory Floor
From low minimum order quantities to full-package cut and sew private labeling, we eliminate supply chain volatility for growing apparel brands.
Low MOQ Production Scaling
Unlike conventional factories demanding 1,000+ units per style, our lines are optimized for 50 to 100-piece low minimums. Test market appetite across multiple colorways without locking capital in dead inventory.
Full Private Label Package
We supply retail-ready garments complete with custom woven neck tags, printed care labels, customized hangtags, branded polybags, and barcoded outer shipper boxes for immediate 3PL fulfillment.
End-to-End Quality Guarantee
Every single batch undergoes rigorous inline and post-production inspection. We pull seams, verify print cure under high-temperature washes, and double-check size ratios against master CAD tech packs.
Precision Cut & Sew Craftsmanship
Master pattern makers convert your basic sketches or tech packs into digitized CAD patterns with precise seam allowances, ensuring perfect fit consistency across repeat restocks.
Tracked International Freight
With operational hubs in Charlotte, NC and Los Angeles, CA, alongside our overseas manufacturing facilities, we deliver door-to-door with complete export clearance documentation.
Firm Timeline Commitments
Sampling is finalized in 20 to 25 business days, followed by bulk production in 25 to 30 business days post sample sign-off. Production slots are locked at booking.
Future Sourcing & Product Development Trends in Custom Wear
Strategic foresight for procurement managers: How digital pattern engineering, sustainable textiles, and smart performance knits are reshaping the global apparel landscape.
1. Circular Economy & Bio-Based Synthetics
The global textile sector is accelerating away from virgin petroleum-based synthetics. Sourcing strategies for 2025 and beyond heavily favor GOTS-certified organic cotton, recycled polyester (rPET) derived from post-consumer ocean plastics, and bio-degradable elastane blends. Incorporating eco-friendly materials not only ensures compliance with upcoming EU Digital Product Passport mandates but also captures premium consumer willingness-to-pay.
2. 3D Digital Twin Prototyping & CAD Precision
Traditional sample iterations often delay product launches by 6 to 8 weeks. Modern CE-certified apparel factories utilize 3D CAD digital twin simulation software to model fabric drape, stretch coefficient, and stress points prior to cutting physical cloth. This technology reduces physical sampling cycles by up to 65%, dramatically lowering development costs and accelerating speed-to-market.
3. Anti-Microbial & Thermoregulatory Smart Textiles
Consumer expectations for everyday and athletic apparel have shifted toward functional utility. High-density 200-needle knitting, integrated silver-ion anti-bacterial treatments, micro-mesh capillary ventilation, and targeted arc compression are becoming standard specifications in high-performance socks, activewear, and athletic teamwear.
4. Supply Chain Agility & Nearshoring Hybrids
To hedge against global geopolitical disruptions, leading apparel brands are adopting hybrid manufacturing models. Combining offshore bulk fabric milling with onshore/nearshore rapid customization and drop-shipping allows brands to maintain healthy gross margins while remaining responsive to rapid micro-trend demand spikes.
8-Stage Standard Operating Procedure: From Tech Pack to Carton Delivery
Transparency at every milestone. Here is how your custom wear order moves across our factory floor.
Consultation
We review your brand concepts, target retail pricing, material preferences, and delivery timeline before issuing a comprehensive formal quotation.
CAD Mockups
Your sketches or tech packs are converted into precise, scaled vector CAD drawings specifying exact measurement points and seam tolerances.
Fabric Sourcing
GSM weight, stretch memory, hand feel, and dye lots are meticulously matched to your approved specs and target profit margin.
Prototyping
A physical fit sample is produced and delivered for hands-on wear testing, allowing pattern refinements prior to bulk fabric cutting.
Cutting & Sewing
Graded master patterns are cut with automated precision cutters and hand-stitched by skilled machinists using high-tenacity thread.
Decoration
Custom artwork is applied via high-density screen printing, 3D puff embroidery, or all-over dye sublimation, followed by thermal curing.
AQL Inspection
Every piece is checked for measurement accuracy, stitch integrity, color fastness, and print durability under strict AQL 2.5 guidelines.
Packing & Ship
Garments are polybagged, customized with hangtags, boxed in heavy-duty export cartons, and shipped with real-time tracking.
Frequently Asked Questions for B2B Custom Wear Sourcing
Direct technical answers addressing minimum order quantities, lead times, certification documentation, and custom branding options.
Ready to Scale Your Apparel Line With a Certified Exporter?
Connect directly with our engineering and procurement team in Charlotte and Los Angeles. Receive instant fabric swatch recommendations, tech pack audits, and transparent wholesale pricing.